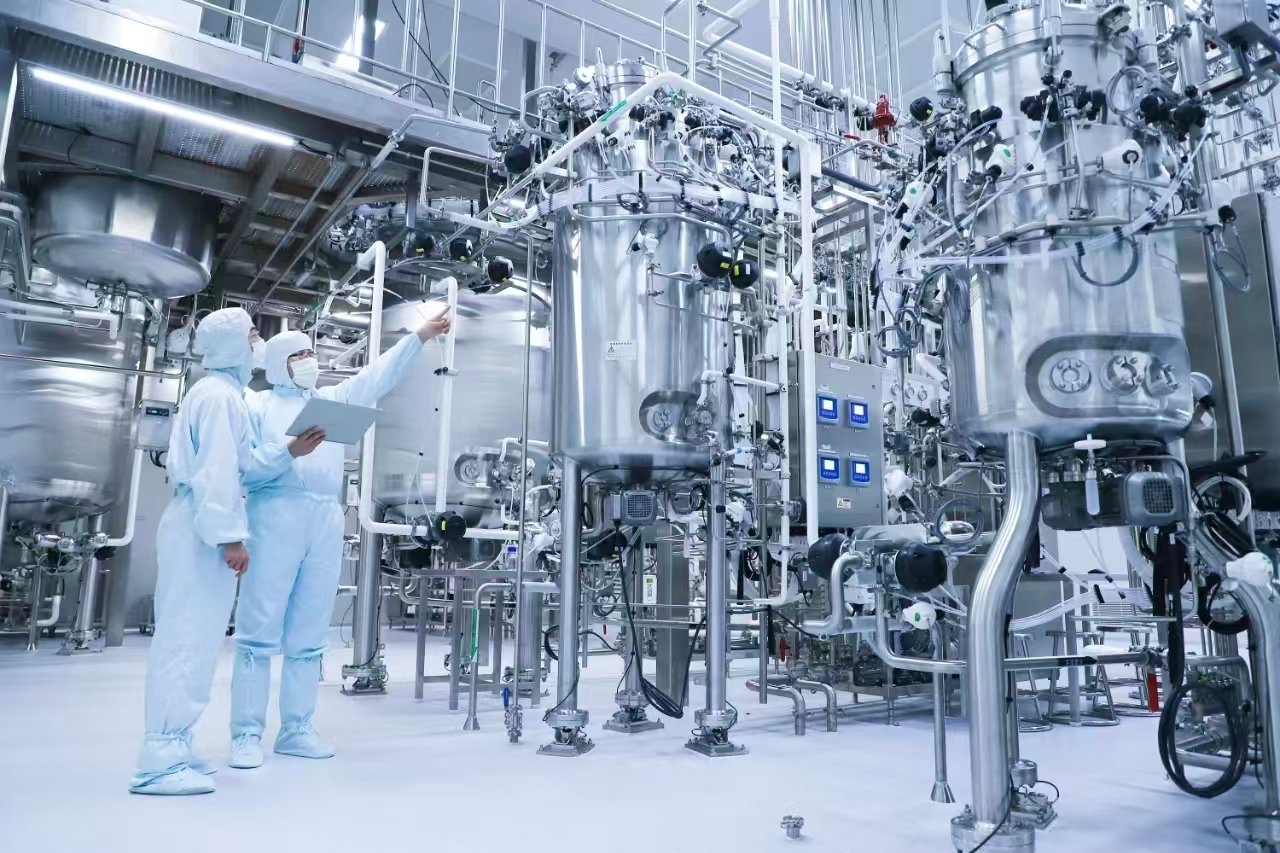
1. Product Positioning & Industry Overview
Engineered for high-purity, scalable commercial production of synthetic and biosynthetic bioactive molecules, our Peptide Manufacturing Plant and Facility Turnkey Engineering Solutions deliver full-lifecycle, process-embedded EPC services for GMP-compliant pharmaceutical, healthcare and cosmetic peptide manufacturing campuses. As the foundational systematic infrastructure that defines production cleanliness, molecular stability, purification consistency and regulatory compliance of peptide-based bioproducts, our integrated design-and-build model resolves critical industry pain points including disorganized process zoning, uncontrolled cross-contamination risks, low purification efficiency, unstable batch quality and fragmented multi-stage production coordination. Tailored for pharmaceutical-grade therapeutic peptides, functional oligopeptides, cosmetic bioactive peptides and nutritional peptide raw materials, our engineering framework fully conforms to FDA, EU GMP and global biomanufacturing standards, supporting clients from site layout planning, process route optimization and cleanroom design to full construction, system commissioning and audit-ready project delivery.
2. Core Design & Technical Framework
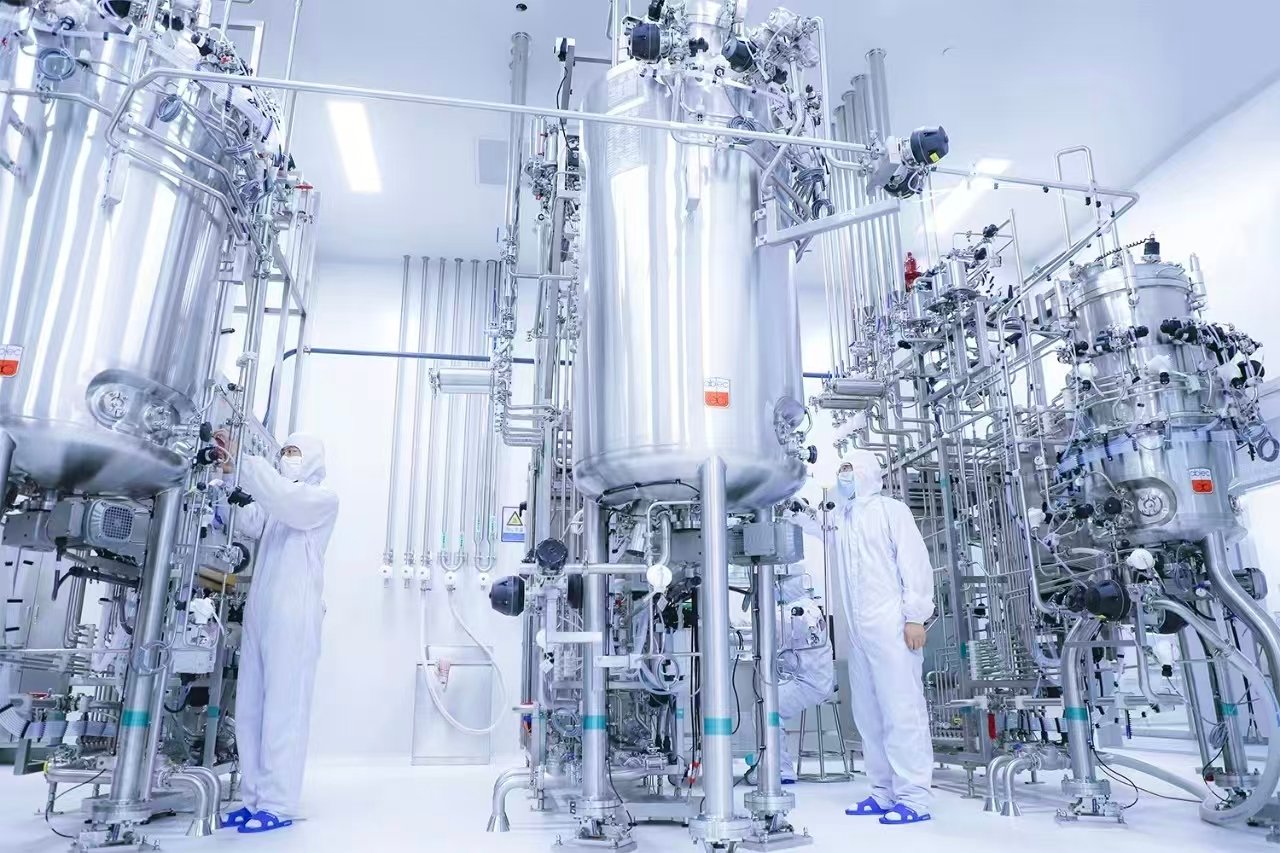
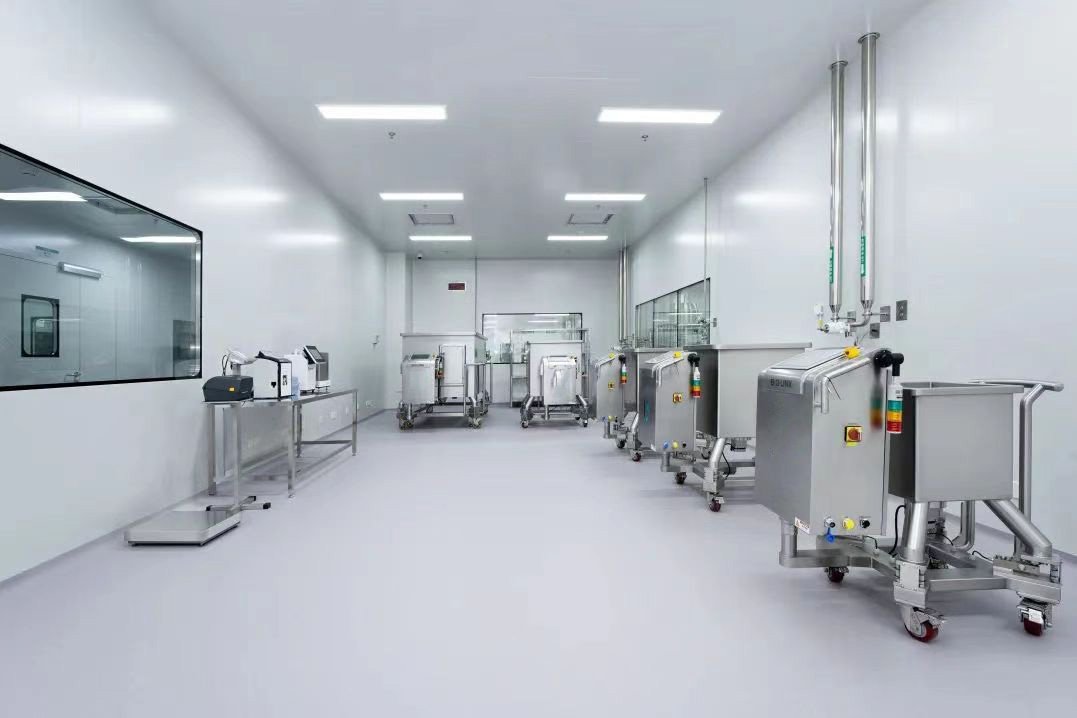
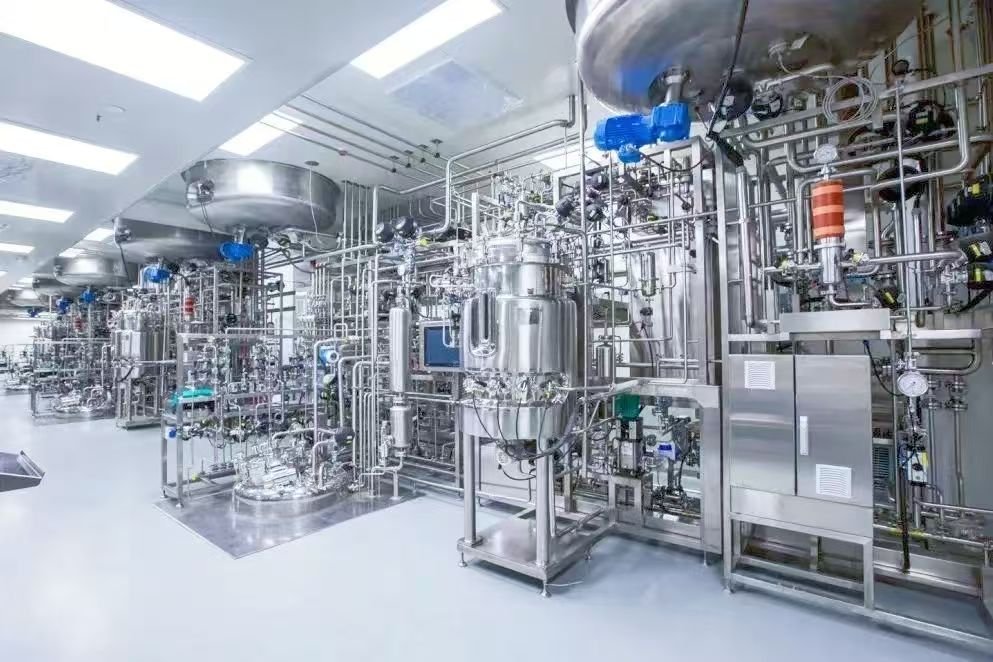
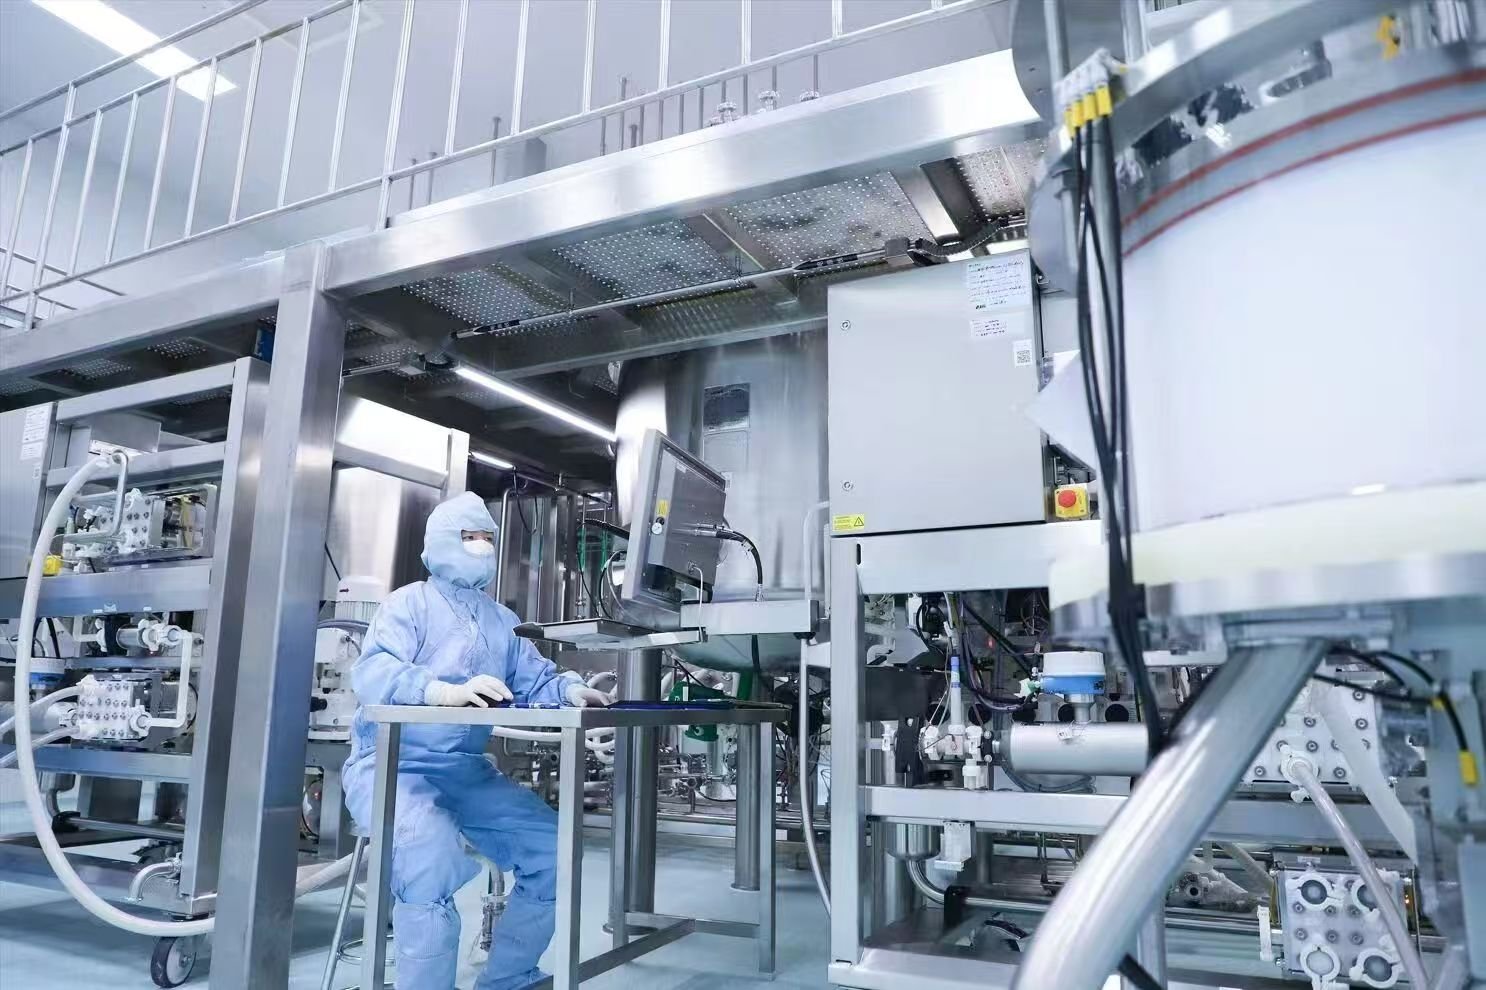
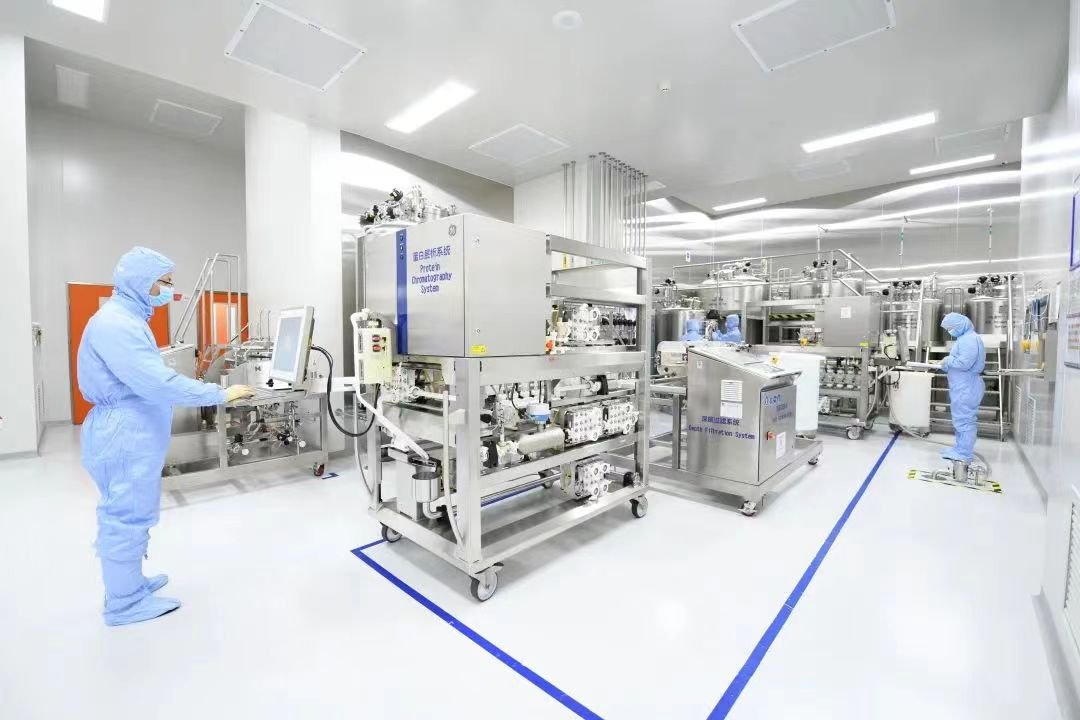
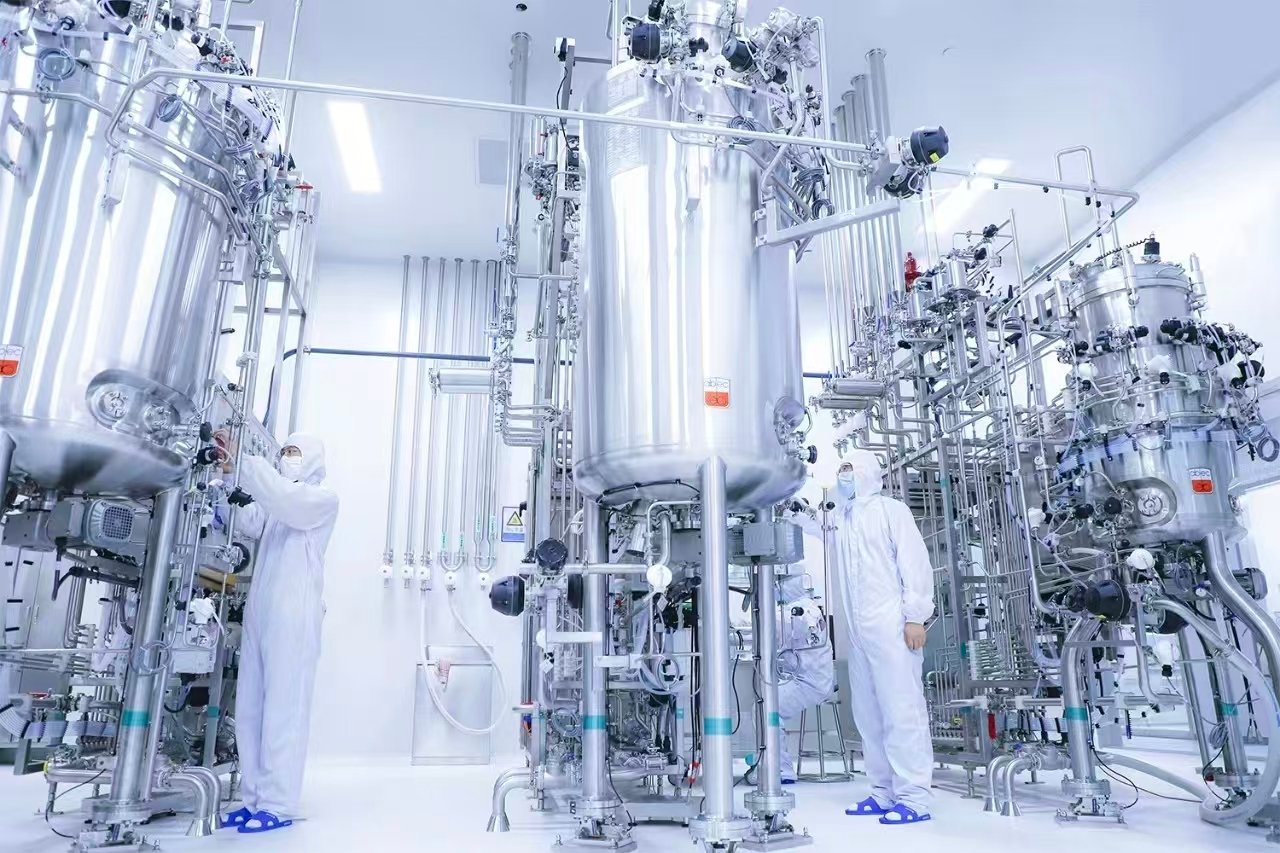
Adhering to stringent Quality by Design (QbD) principles and high-standard fine biomanufacturing specifications, our full-scope turnkey engineering covers complete facility architectural design, classified cleanroom grading, HVAC environmental control, ASME BPE-grade sanitary utility systems, closed synthetic and fermentation process layout, multi-stage downstream purification zoning, intelligent process monitoring and auxiliary facility integration. We implement rigorous functional partitioning and hierarchical contamination prevention strategies to fully isolate peptide synthesis, microbial fermentation, crude extraction, chromatographic refining, membrane purification, concentration and aseptic packaging zones, effectively eliminating exogenous impurity intrusion, cross-contamination and molecular degradation risks. The entire facility adopts modular, low-temperature and low-shear process-oriented design logic, reserving flexible expansion space for product iteration and capacity scaling while maintaining full compatibility with automated production systems, integrated CIP/SIP units and data integrity management platforms, forming a precise, stable and fully compliant closed-loop peptide manufacturing system.
3. Premium Performance & Technical Advantages
Distinct from conventional general bioprocess facility engineering lacking peptide-specific technical pertinence, our professional turnkey solution delivers superior advantages in molecular activity retention, purification accuracy, operational stability and regulatory adaptability. The process-customized facility layout realizes precise matching between environmental parameters and peptide production characteristics, avoiding quality fluctuations, molecular denaturation and process bottlenecks caused by unreasonable facility design. Optimized closed and low-temperature production workflows significantly improve product purity and batch-to-batch reproducibility while reducing active ingredient loss throughout downstream processing. All design documents, engineering validation dossiers, sanitary control protocols and project acceptance deliverables strictly comply with cGMP, FDA and EU GMP regulatory mandates, enabling efficient third-party audit clearance and global market access qualification. Standardized modular EPC implementation shortens project lead times, minimizes on-site modification risks, and reduces long-term operational energy consumption and lifecycle maintenance costs.
4. Application Value & Industrial Empowerment
Our peptide manufacturing facility turnkey engineering serves as the core infrastructure guarantee for standardized, high-efficiency and compliant industrialization of high-value bioactive peptide products. Widely applicable in greenfield peptide plant construction, existing fine biomanufacturing workshop renovation, pharmaceutical peptide production upgrading and high-end bioactive raw material industrial base deployment, our integrated EPC services help enterprises build low-risk, high-precision and audit-optimized peptide manufacturing environments. By optimizing full-process production logic, realizing seamless linkage between upstream synthesis/fermentation and downstream fine purification systems, and standardizing whole-chain quality control and compliance management mechanisms, we effectively reduce production costs and project investment risks. This empowers biomanufacturing enterprises to accelerate product commercialization, achieve flexible capacity expansion and diversified product iteration, and establish sustained core competitiveness in the global high-end peptide and fine biopharmaceutical manufacturing market.