

1. Solution Overview & Global GMP Compliance Framework
Our process‑driven bioprocessing engineering solutions are purpose‑built for end‑to‑end monoclonal antibody manufacturing, complying strictly with FDA cGMP, EMA Annex 1, PIC/S PI 006‑4 and ICH Q8/Q9/Q10 quality risk‑management standards. The scope covers upstream cell culture, harvest clarification, multi‑step downstream purification, viral clearance, sterile formulation and supporting utility infrastructure, supporting fed‑batch, high‑titer and perfusion‑based mAb workflows. Rather than applying generic plant templates, every engineering decision originates from mAb‑specific critical process parameters (CPPs) and critical quality attributes (CQAs), addressing typical industry pain‑points including mismatched upstream‑downstream capacity, inconsistent titer output, excessive product loss during purification, ineffective contamination control and heavy validation burdens. The solution serves greenfield commercial facilities, brownfield plant retrofits and compact clinical pilot manufacturing suites for biotech enterprises and CMO operators worldwide.
2. Core Engineering Philosophy & mAb‑Focused Technical Advantages
Guided by risk‑based contamination mitigation and deterministic process realization, layout, equipment sizing, utility configuration and automation logic are all derived from actual mAb process characteristics via upfront FMEA risk assessment.
1,Balanced upstream‑downstream capacity matching Equipment volume, flow rates and material transfer paths are dimensioned according to target bioreactor output, eliminating bottlenecks between cell culture harvest and subsequent capture chromatography and avoiding over‑sized redundant hardware.
2.Protein‑friendly sanitary process design Low‑shear fluid architecture is adopted across bioreactors, transfer loops and purification skids to reduce antibody aggregation; 316L stainless‑steel wetted surfaces with Ra ≤ 0.4‑0.6 μm finish and zero‑dead‑leg piping minimise residual mAb buildup and biofilm formation for reliable cleaning validation.
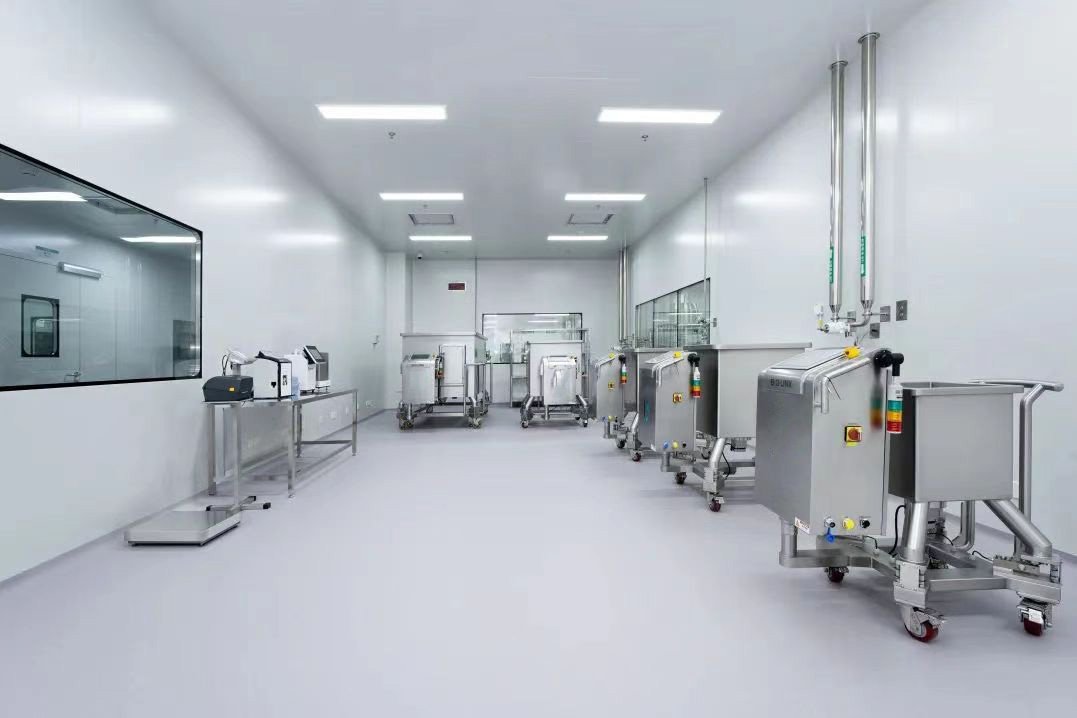
3.Unidirectional material‑personnel‑waste flow zoning Linear process‑oriented cleanroom zoning separates seed expansion, main cell culture, purification and formulation zones with physical barriers and pressure cascades, lowering cross‑contamination risk between different mAb batches or product lines.
4.Process‑embedded automated control strategy Integrated PAT‑ready automation platform implements closed‑loop control for cell culture parameters, chromatography gradient elution and TFF buffer‑exchange steps, with immutable electronic batch records to satisfy global data‑integrity requirements. Compared with architecture‑first conventional designs, this process‑driven approach improves overall mAb yield, stabilises product quality consistency and reduces long‑term operational and validation costs.
3. Four Integrated Engineering Modules & Standard Deliverables
The complete mAb‑focused bioprocessing engineering system consists of four tightly‑coordinated functional modules covering the full mAb manufacturing value‑chain: upstream cell‑culture engineering module, harvest‑to‑purification downstream engineering module, sterile formulation & intermediate storage module, and supporting utility‑automation & compliance documentation module.
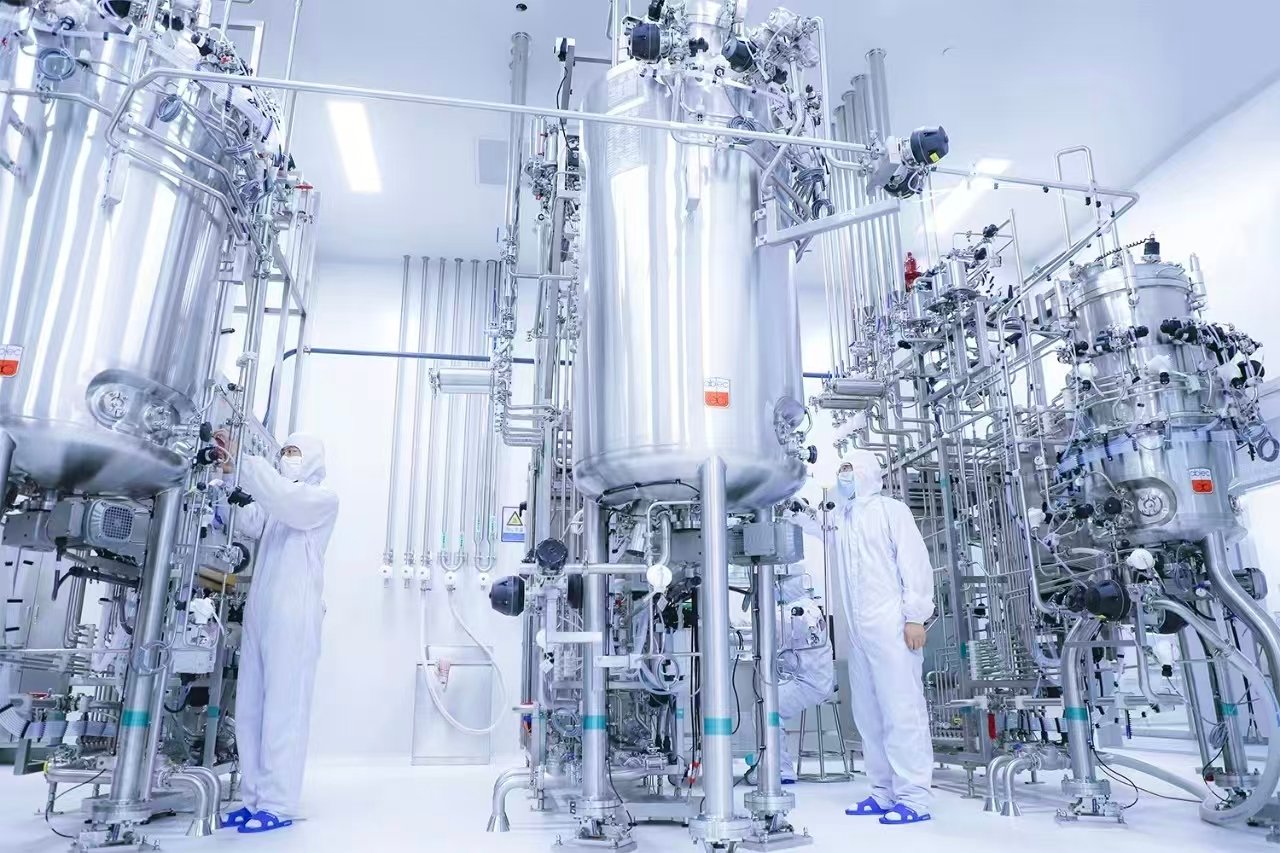
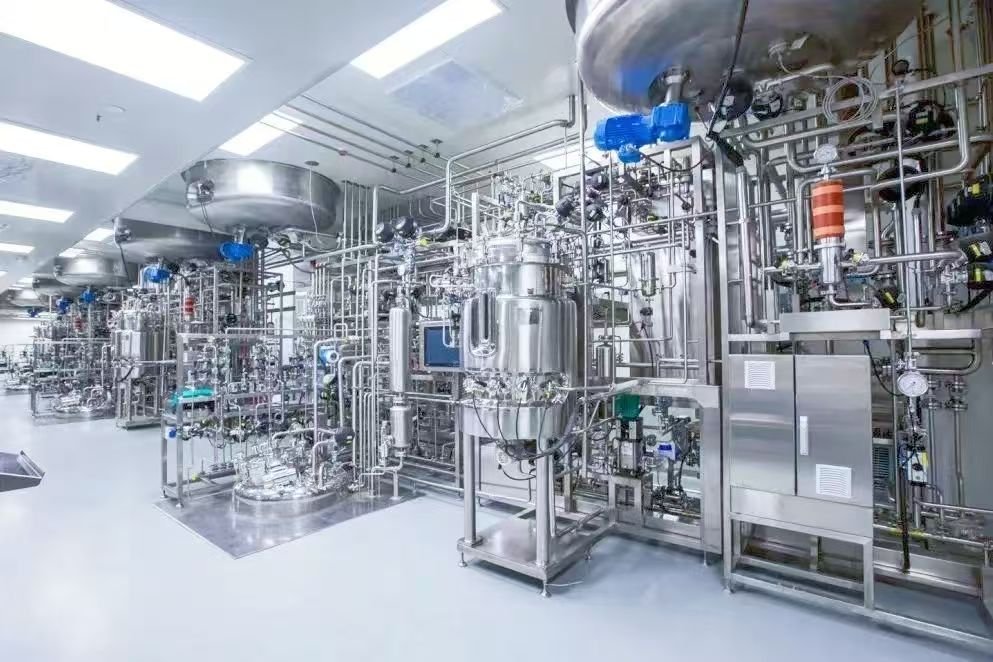
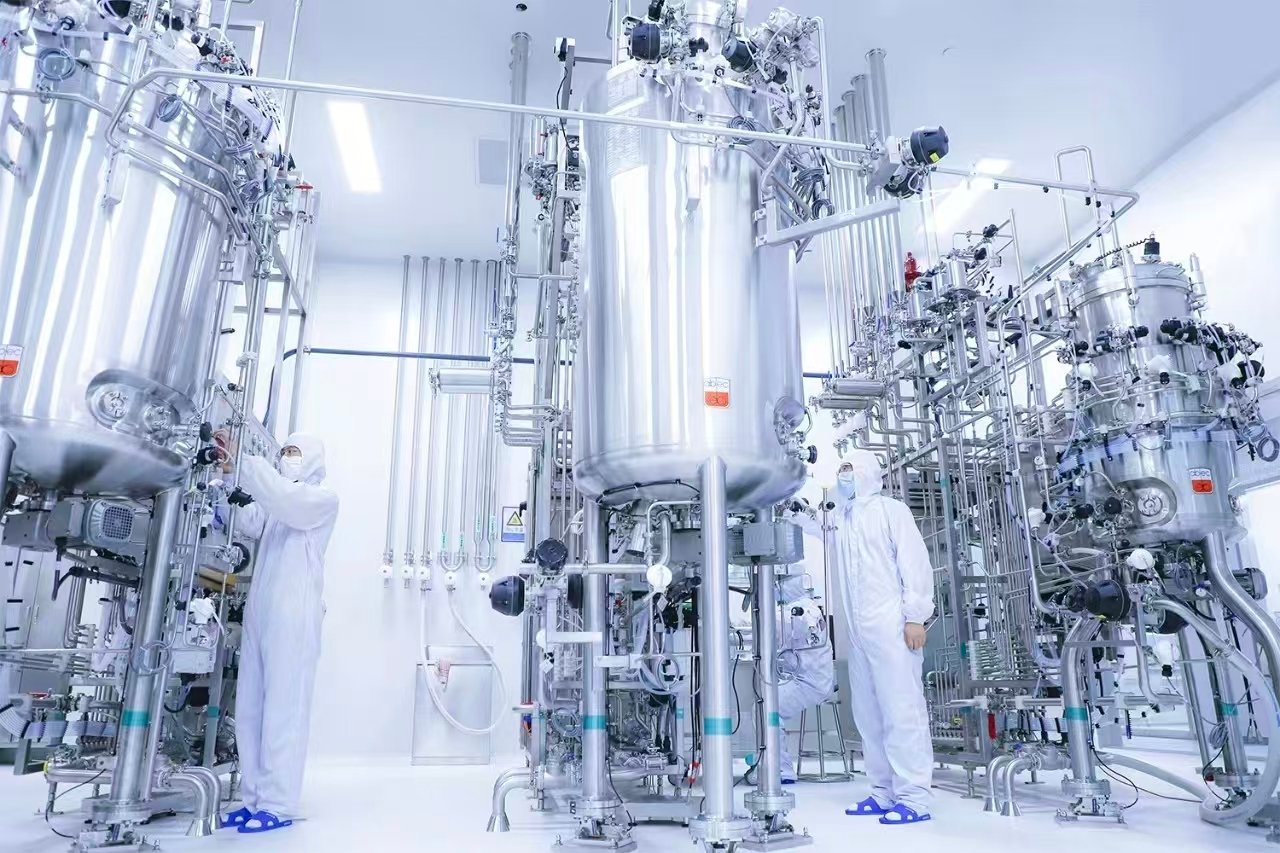
1.Upstream Cell‑Culture Engineering Module Deliver process‑matched bioreactor systems for fed‑batch or perfusion operation, together with medium‑and‑buffer preparation suites, seed‑bank supporting cold‑rooms and dedicated exhaust‑treatment systems. Output URS, layout drawings and DQ documents optimised for high‑density mammalian cell culture and high‑titer mAb expression.
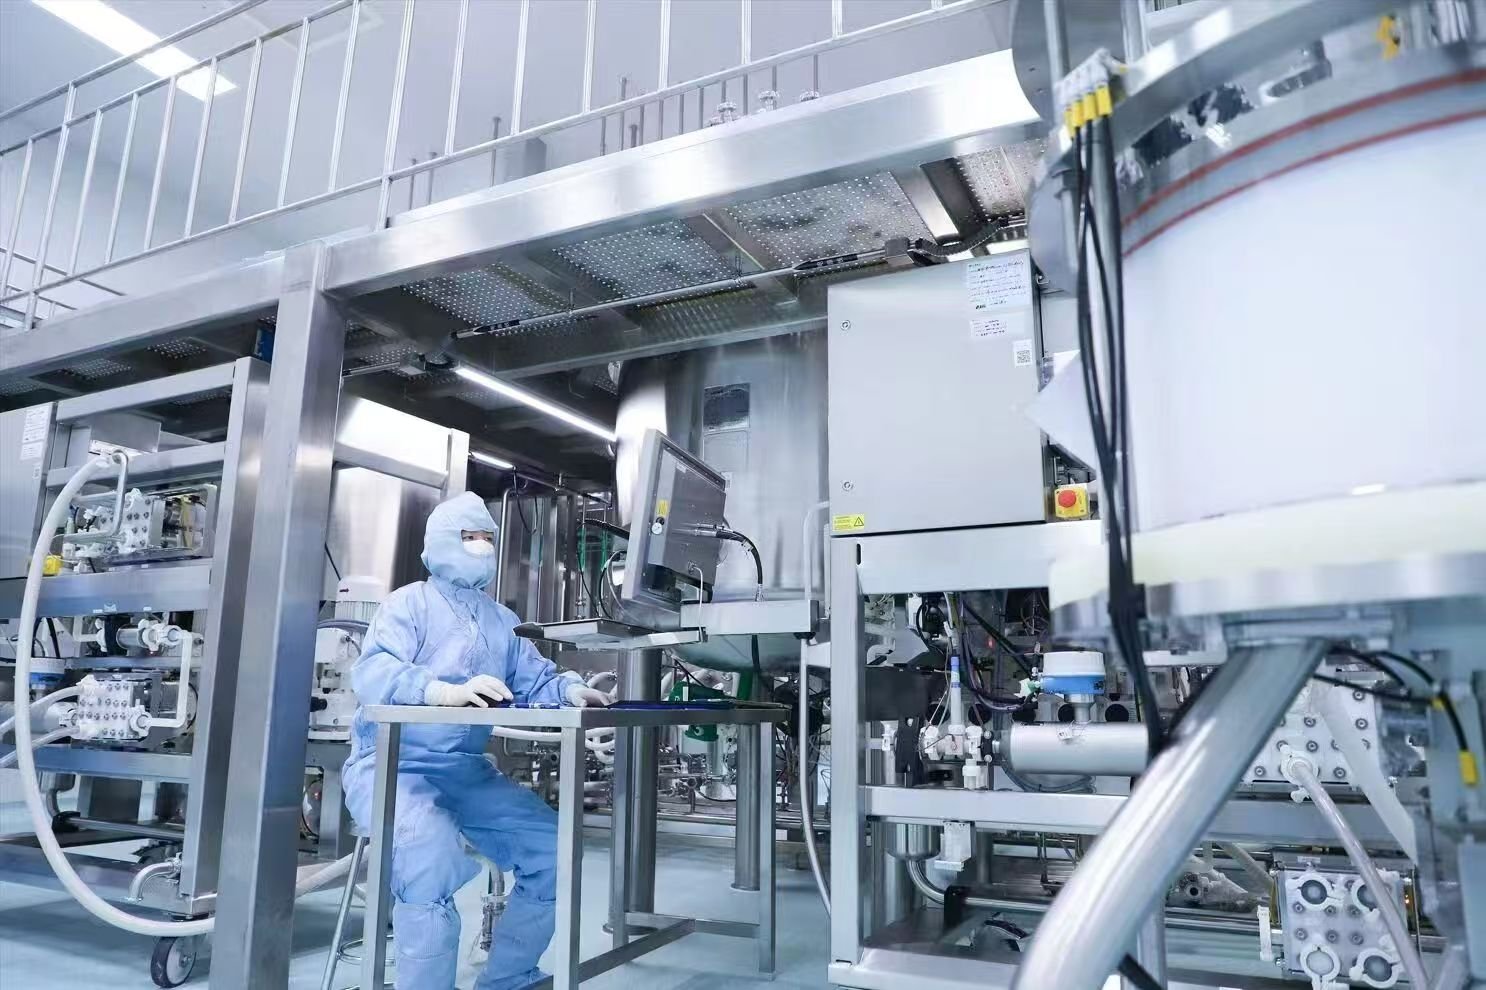
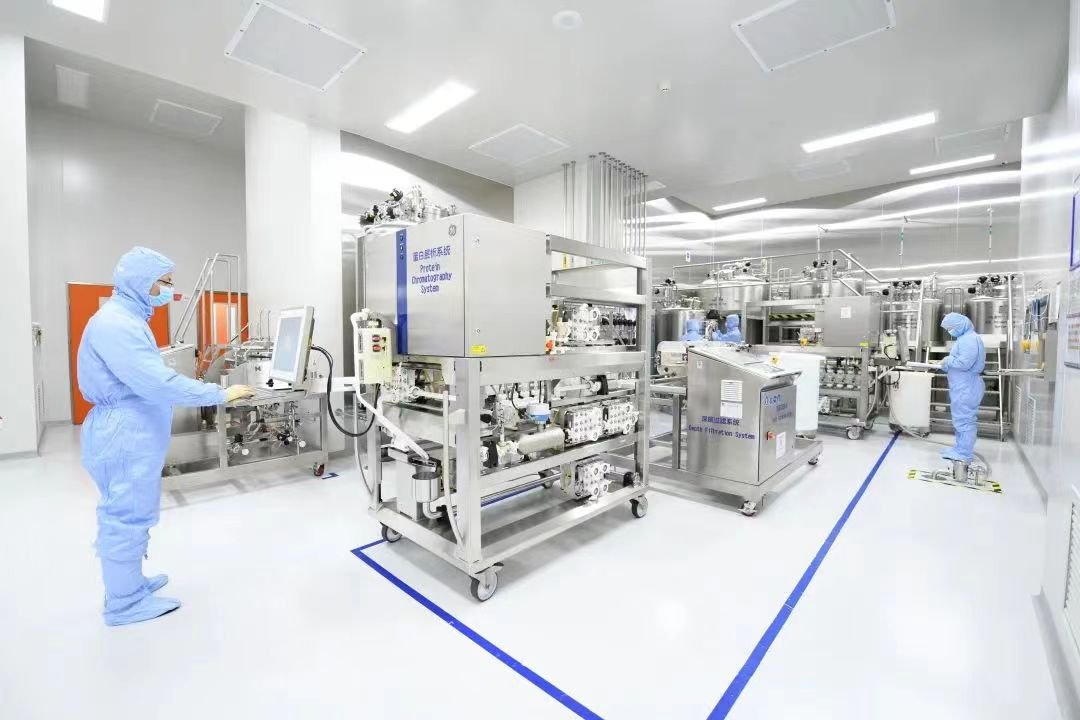
2.Harvest‑to‑Purification Downstream Engineering Module Integrate customized clarification, protein‑A capture, intermediate polishing, virus inactivation, virus filtration and UF/DF buffer‑exchange skids; configure closed transfer pipelines and dedicated CIP/SIP circuits for multi‑product switching. Provide cleaning‑validation master plans aligned with mAb impurity‑removal requirements.
3.Sterile Formulation & Intermediate Storage Module Set up Grade A/B aseptic formulation zones for mAb drug‑substance bulk; deploy temperature‑controlled sterile holding vessels with full sanitary sterilisation coverage, closed sampling interfaces and segregated cold‑storage areas for drug‑substance intermediates.
4.Utility‑Automation & Compliance Documentation Module Design HVAC clean‑room grading, PW/WFI distribution networks and centralised CIP/SIP systems tailored to mAb workflows; deploy SCADA‑based process‑control systems with audit‑trail functions. Deliver facility risk assessments, contamination‑control strategy and full‑set qualification documents for regulatory audits.
4. Industrial Application & Full Lifecycle Engineering Support
These process‑driven mAb bioprocessing solutions apply to large‑scale commercial mAb greenfield plants, capacity‑expansion or compliance‑retrofit brownfield projects, clinical‑phase pilot production platforms and multi‑product flexible CMO facilities. The modular framework enables scalable expansion: higher titre processes or additional mAb pipelines can be accommodated through module extension without large‑scale facility reconstruction. We provide full‑lifecycle technical services including pre‑project process simulation review, design optimisation, on‑site construction supervision, FAT/SAT support, IQ/OQ/PQ guidance and GMP operational training. By translating mAb process requirements into tangible facility, equipment and control solutions, our engineering services help biopharma clients achieve stable antibody quality, shorten project delivery cycles and accelerate global regulatory approval and commercial launch of monoclonal‑antibody therapeutics.
