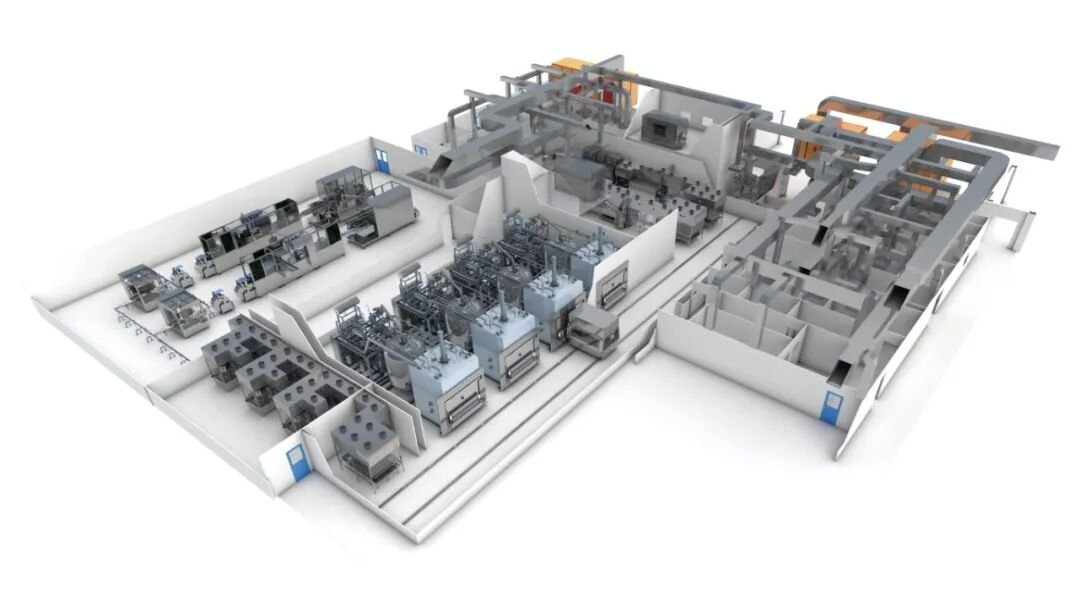
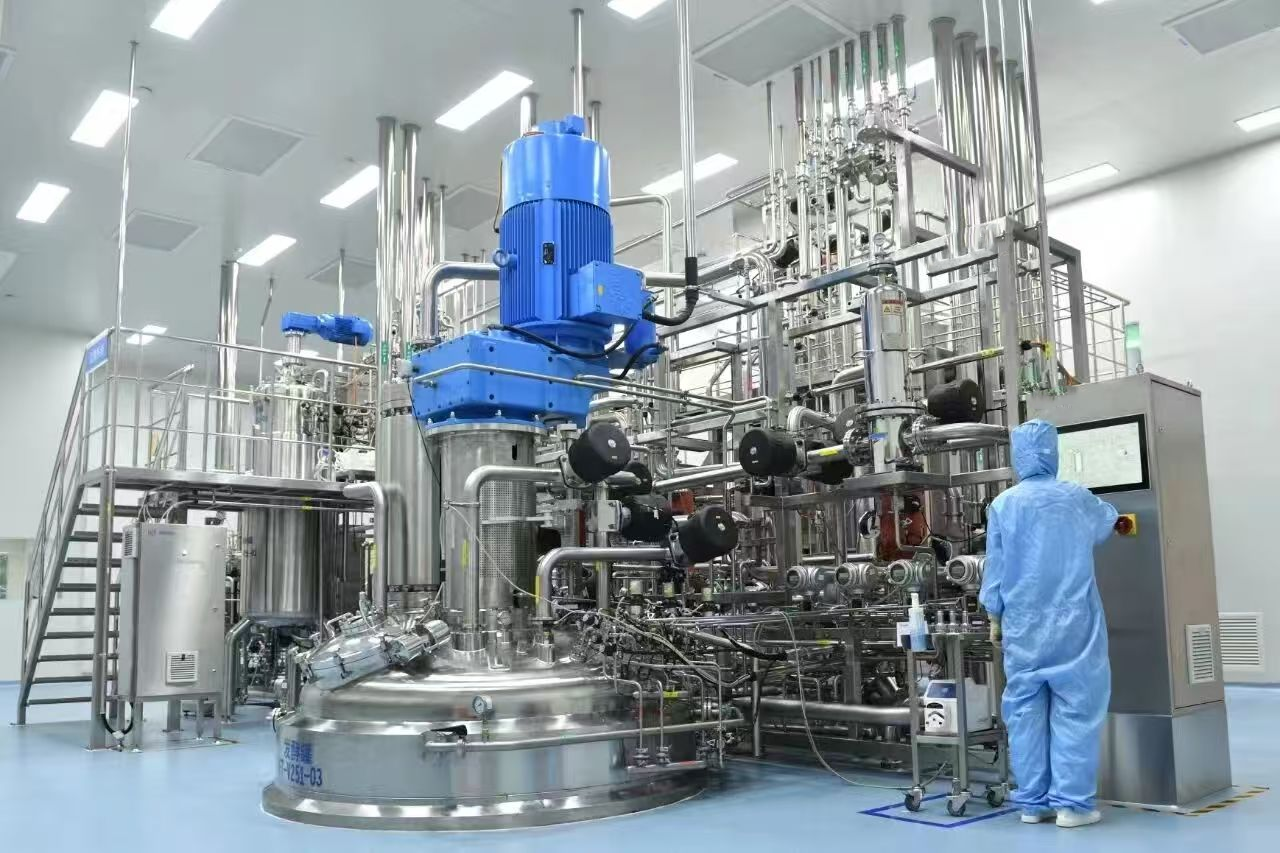
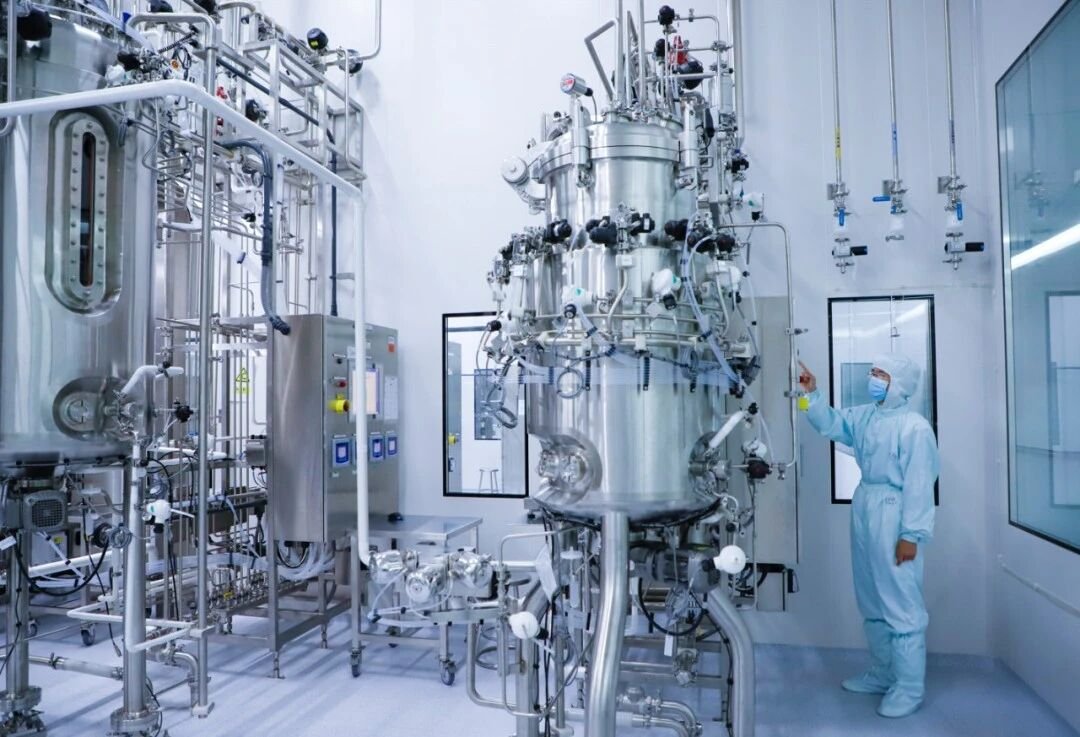
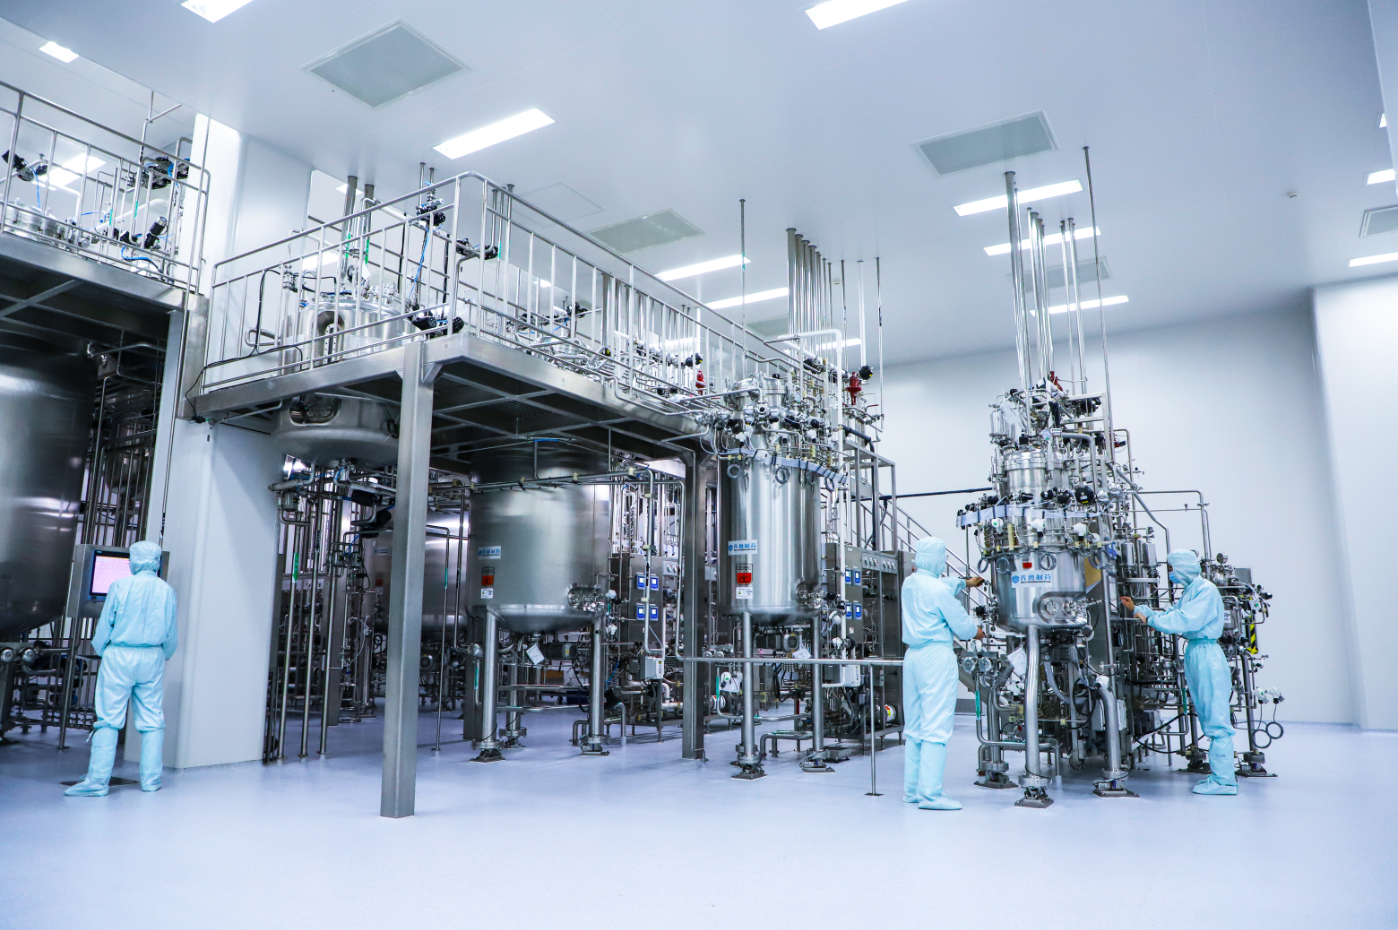
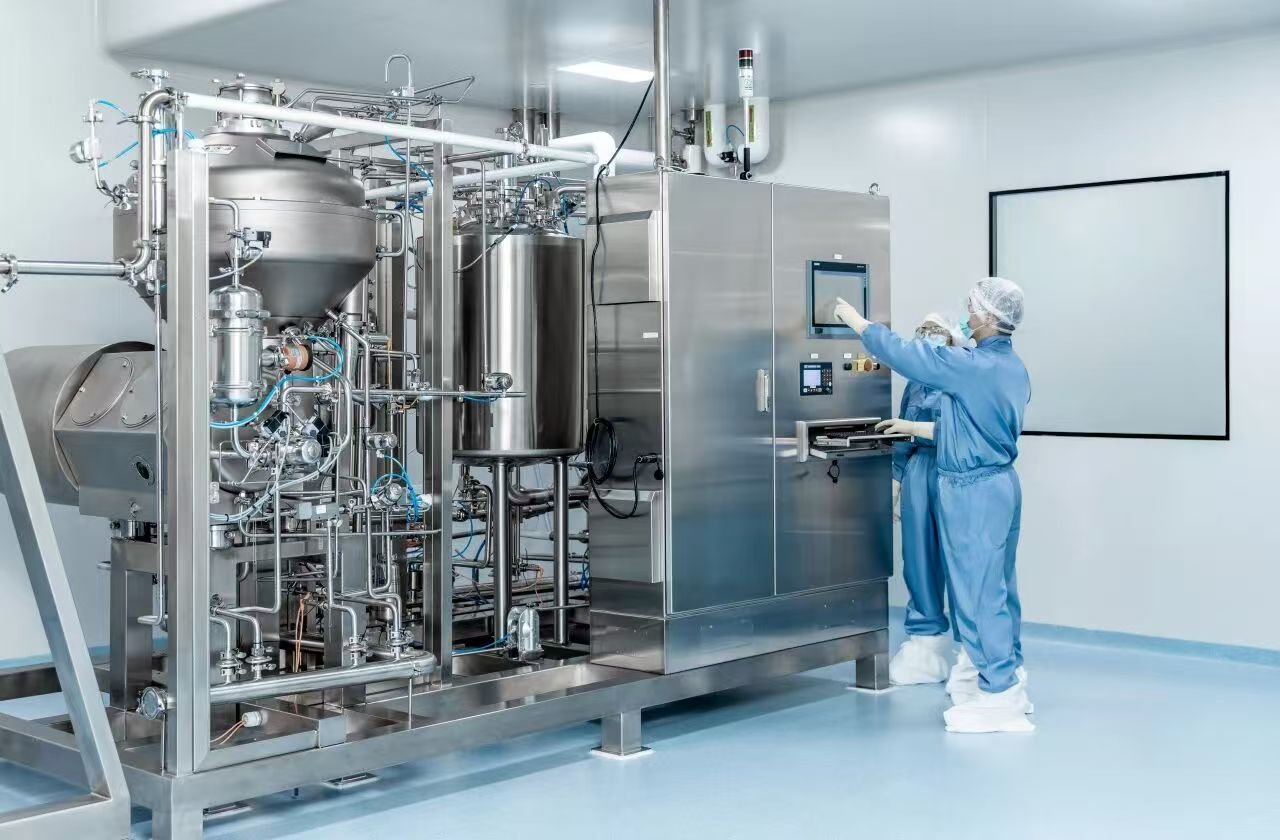
Our biopharmaceutical pilot plant design and scale-up engineering service delivers a strategically engineered bridge between laboratory process development and GMP-compliant clinical and commercial manufacturing. Tailored for monoclonal antibodies, recombinant proteins, viral vectors, cell therapy intermediates and complex biologic modalities, this offering addresses the core technical challenge of translating bench-scale workflows into reproducible pilot operations, with full alignment to ICH, FDA and EU GMP regulatory expectations. We integrate facility layout, classified cleanroom zoning, process utility distribution, skid-based unit operations and automation architecture from the earliest conceptual design phase, embedding flexibility to accommodate iterative process changes, parallel product campaigns and future capacity expansion without costly foundational rework.
Our engineering framework is built upon rigorous scale-up science anchored in hydrodynamic characterization, mass transfer modelling, mixing homogeneity analysis and statistically justified Design-of-Experiments workflows to preserve critical quality attributes across volumetric transitions. We develop quantified scale-up criteria for bioreactor systems, harvest, clarification, chromatography, tangential flow filtration and formulation unit operations, pairing process modelling with P&ID development, equipment specification, sanitary piping design, PAT instrumentation integration and S88-compliant control system architecture. Every subsystem is engineered for seamless technology transfer, with clear definition of critical process parameters, control strategies, sampling regimes and data integrity controls to support regulatory submissions, process characterization and validation master planning.
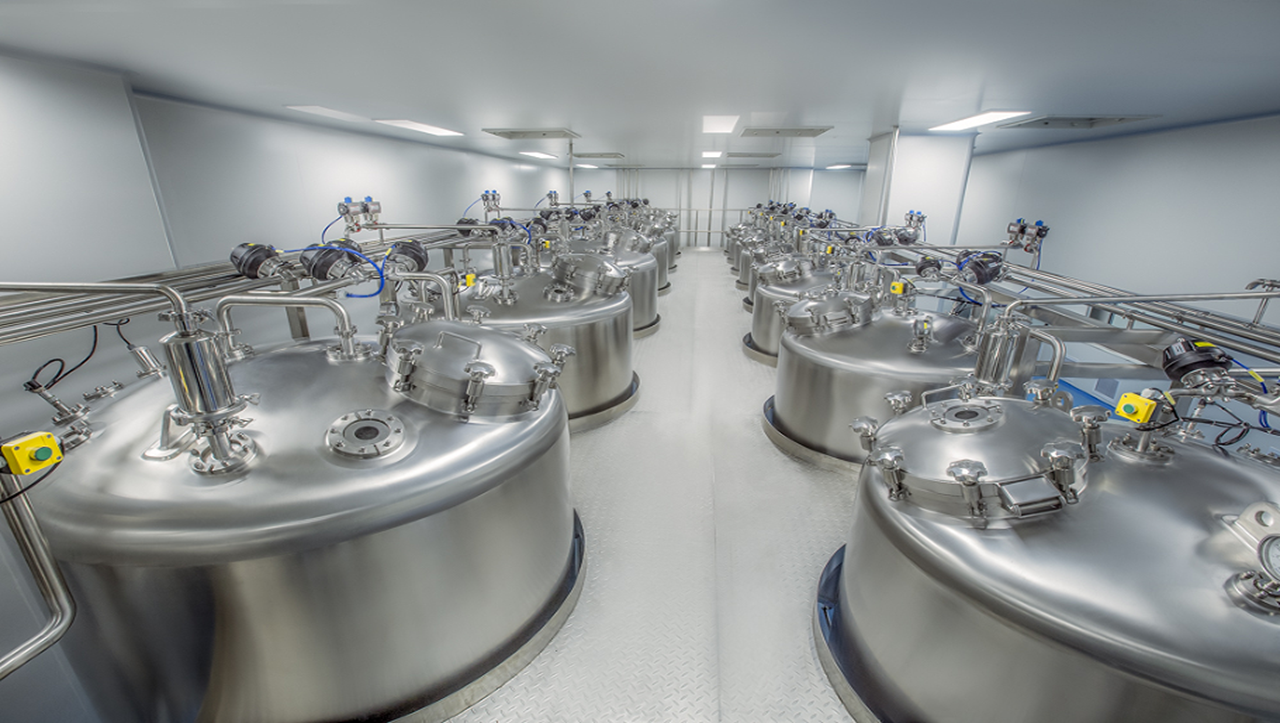
The solution delivers tangible operational and regulatory risk reduction by de-risking scale-dependent failure modes before investment in large-scale production assets. Our modular pilot plant configuration supports rapid reconfiguration between single-use and stainless-steel process trains, reduces validation cycle time, improves batch-to-batch consistency and lowers overall capital expenditure for early clinical material supply. We execute FAT, SAT, commissioning, qualification and performance verification in a structured sequence, while embedding digital traceability to enable continuous process performance monitoring and deviation management. This controlled de-risking pathway shortens CMC timelines, minimises technology transfer variability and prevents costly redesigns at later clinical stages.
We provide end-to-end lifecycle engineering support extending from conceptual design and process scale-up studies through construction oversight, commissioning, qualification and ongoing technical advisory for process optimisation and facility change control. Our cross-functional team of bioprocess engineers, cleanroom specialists, automation architects and regulatory subject-matter experts works closely with sponsors to align pilot plant performance with clinical supply roadmaps and long-term commercial manufacturing targets. Whether for standalone pilot facilities integrated within existing R&D campuses or modular relocatable pilot suites, our engineering output establishes a robust, defensible technical foundation that accelerates biologic development programs while maintaining uncompromised compliance and product safety standards.