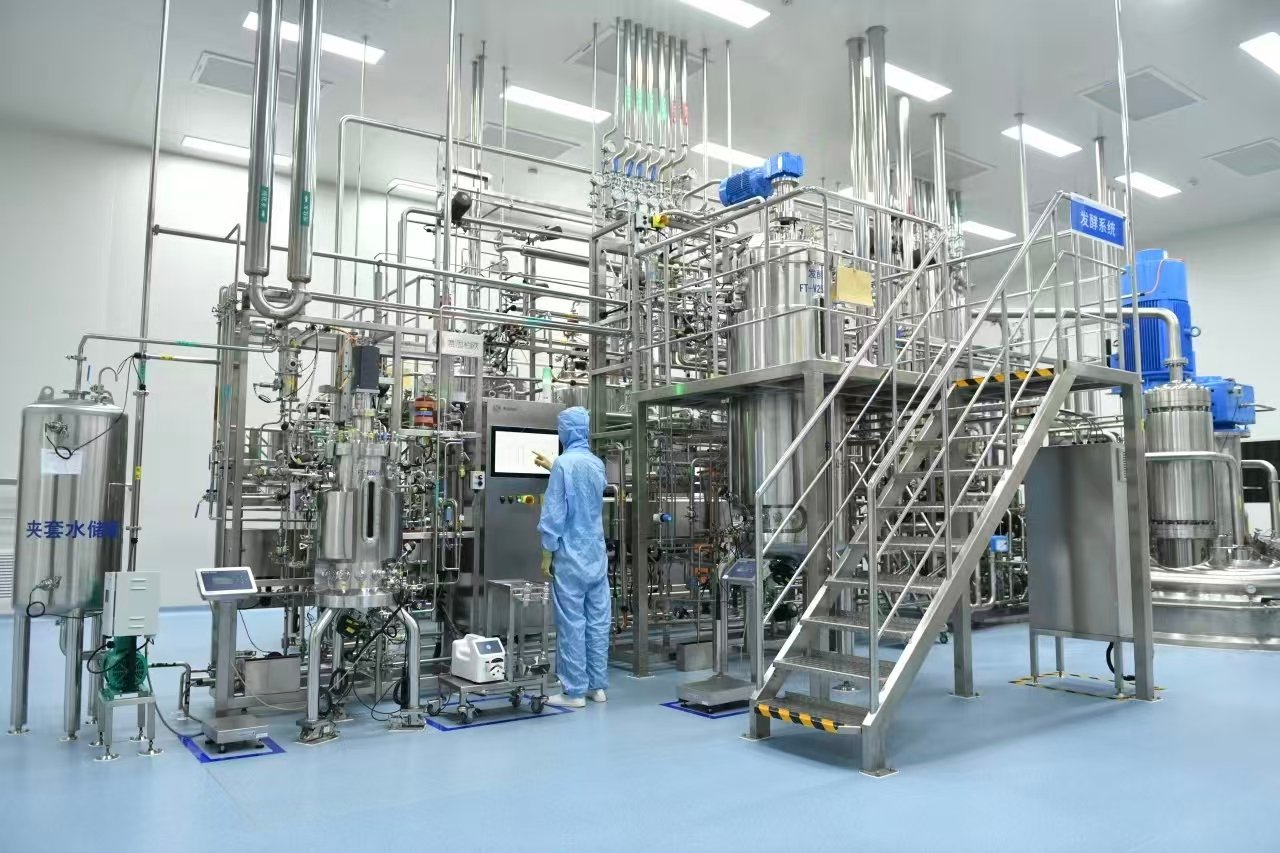
1. Design Overview & Global GMP Compliance Framework
Our specialized bioprocessing equipment design is tailor-engineered for end-to-end recombinant protein manufacturing workflows, covering microbial fermentation, mammalian cell expression, downstream purification, buffer formulation and sterile bulk storage. All design specifications fully comply with FDA cGMP, EMA Annex 1, PIC/S and ICH Q8/Q9/Q10 quality and data integrity standards, adapting to therapeutic proteins, fusion proteins, enzymes, cytokines and vaccine antigen production. Unlike general-purpose bioprocess hardware that ignores protein stability and impurity clearance characteristics, our protein-specific design targets core industrial pain points including excessive protein denaturation, residual host cell impurities, low purification recovery, insufficient sterile protection and poor batch consistency. We deliver audit-ready, process-optimized equipment solutions for laboratory process development, clinical pilot production and large-scale commercial recombinant protein manufacturing sites worldwide.
2. Core Design Philosophy & Recombinant Protein-Specific Advantages
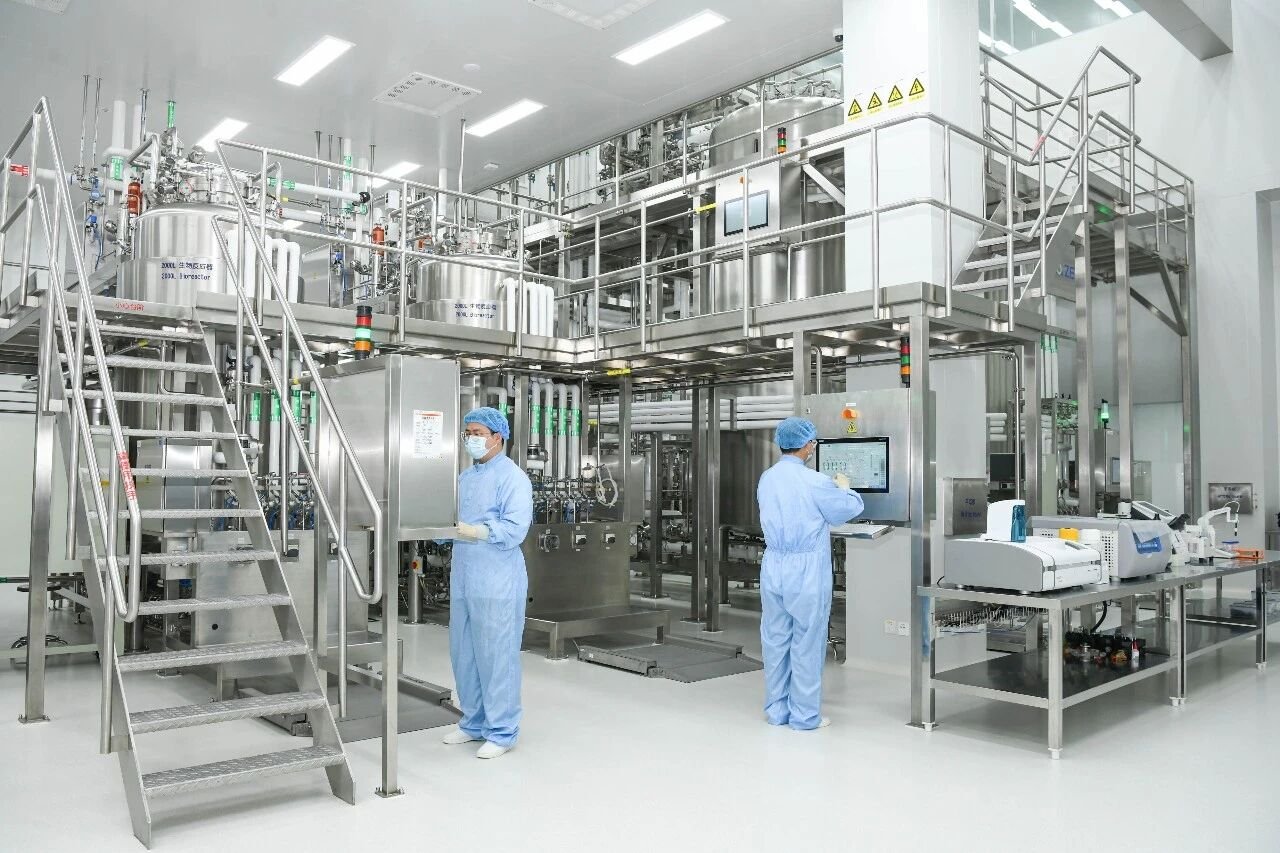
Guided by protein stability protection and risk-based contamination control principles, every structural and functional design is aligned with the unique critical process parameters (CPPs) and critical quality attributes (CQAs) of recombinant protein production. The entire equipment system adopts low-shear hydrodynamic design to prevent protein structural degradation and aggregation during cell culture, pumping and transfer processes. All wetted parts utilize 316L sanitary stainless steel with Ra ≤0.4–0.6 μm mirror polishing and zero-dead-leg layout, eliminating residual protein buildup, biofilm formation and cross-batch contamination. Customized temperature-controlled circulation modules and low-temperature buffer preparation interfaces effectively preserve fragile protein activity, while optimized flow-rate-matched piping and skid structures reduce product hold-up and maximize purification yield. Compared with universal equipment designs, our recombinant protein-focused configuration delivers higher process reproducibility, lower impurity levels and superior long-term cleaning validation stability for consistent protein quality output.
3. Four Core Customized Equipment Design Modules & Standard Deliverables
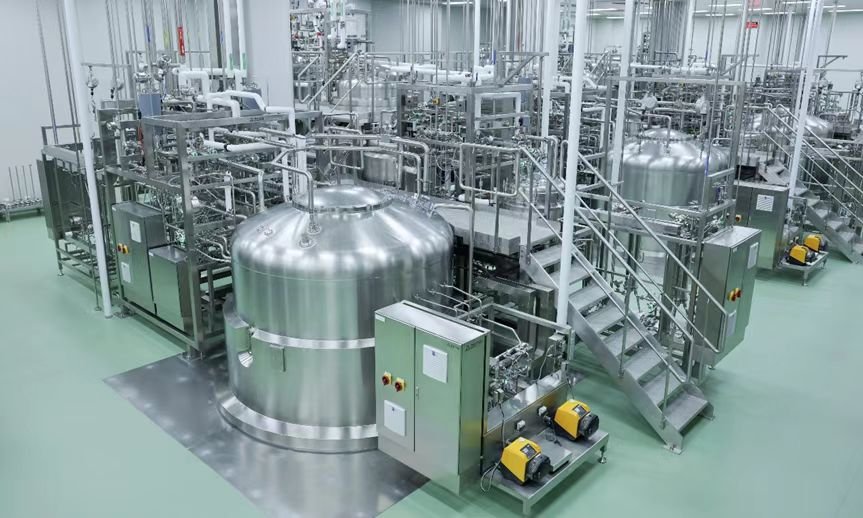
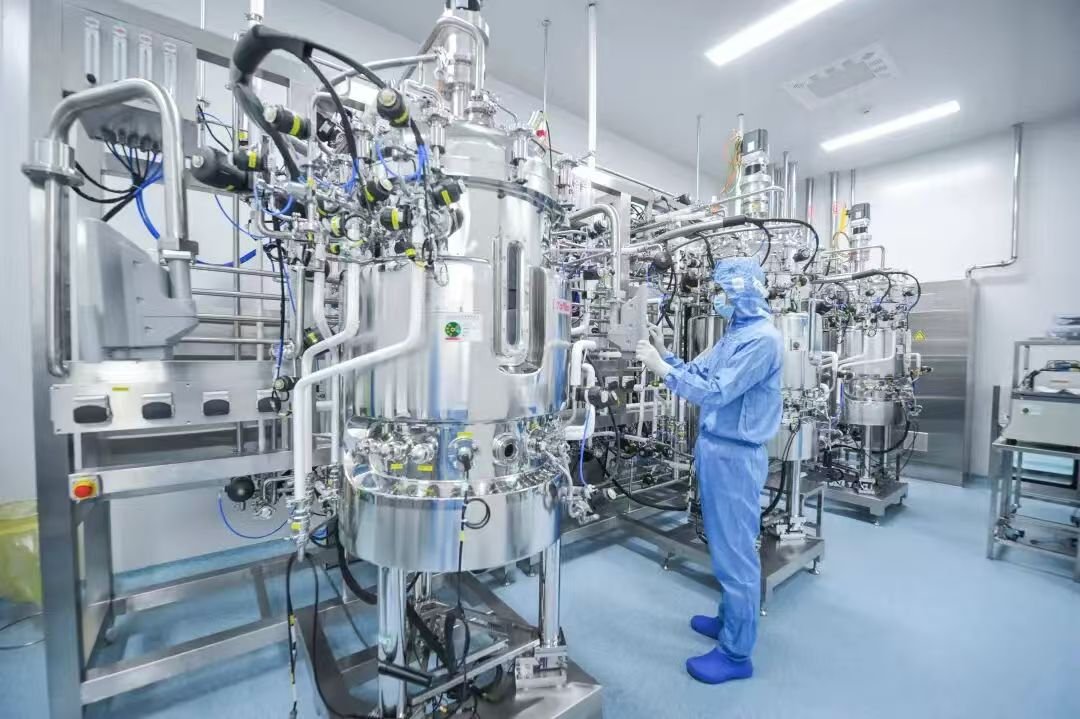
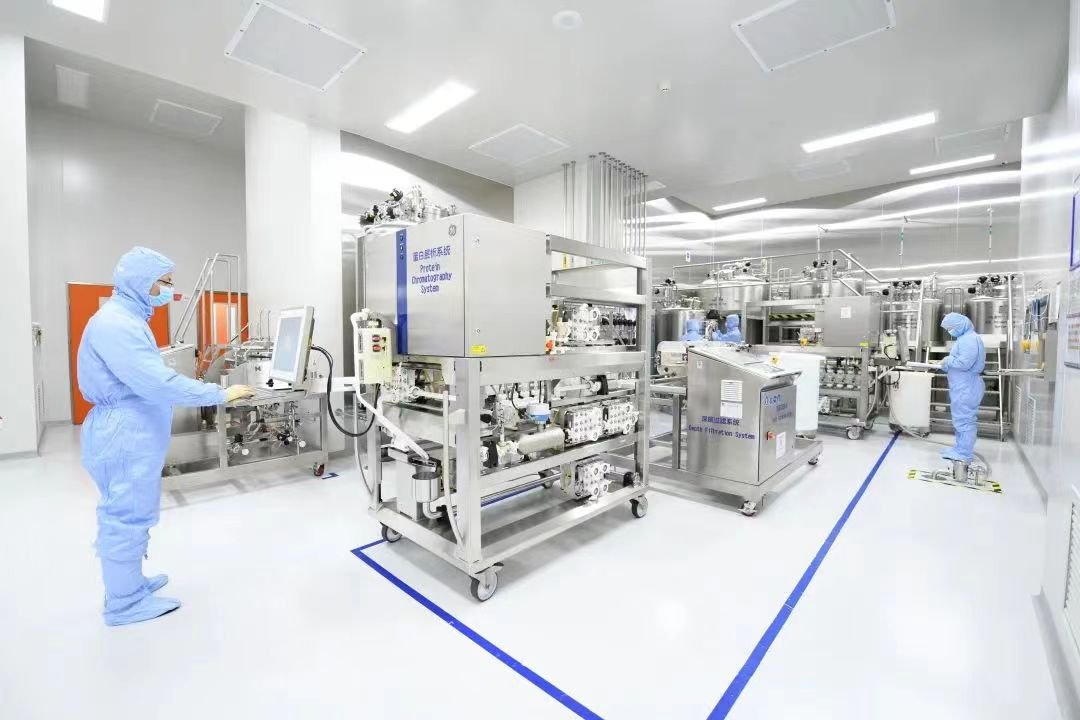
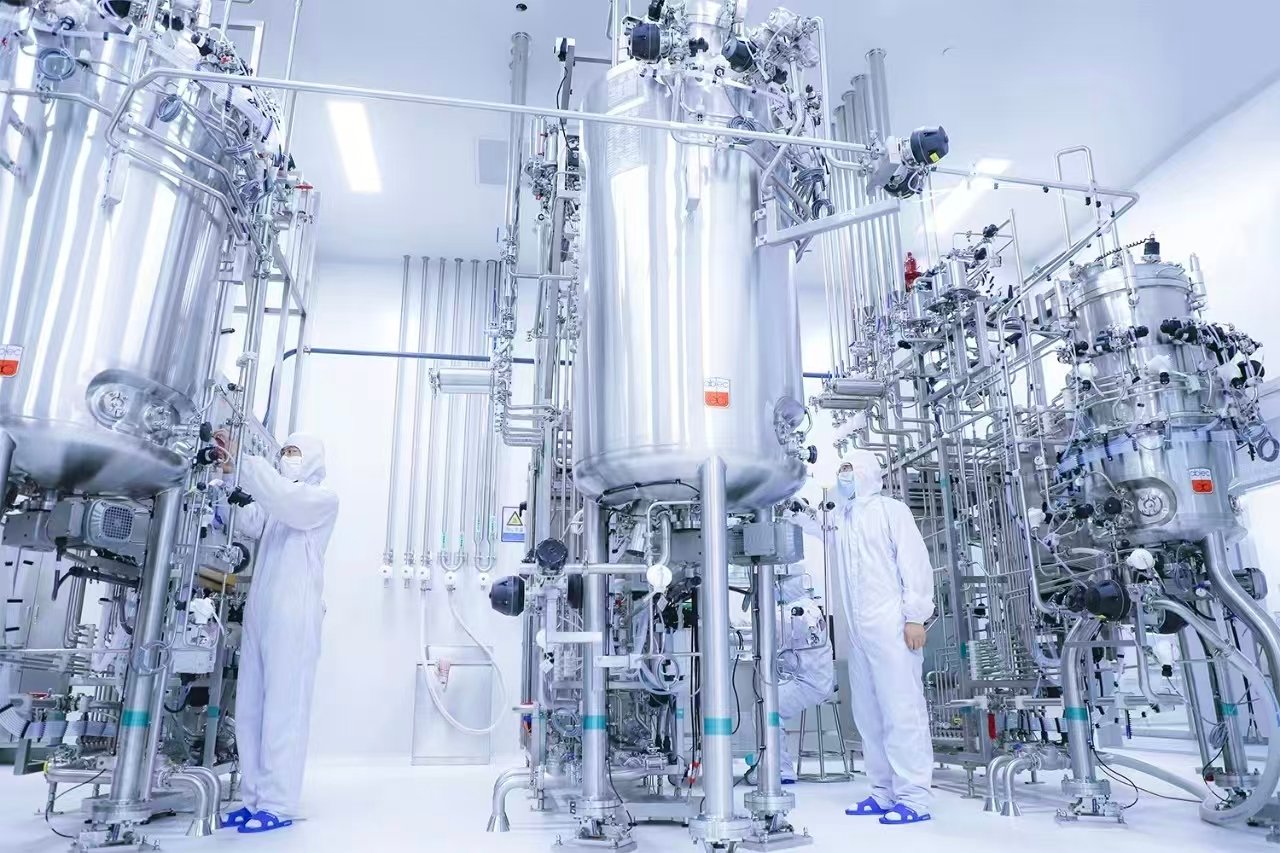
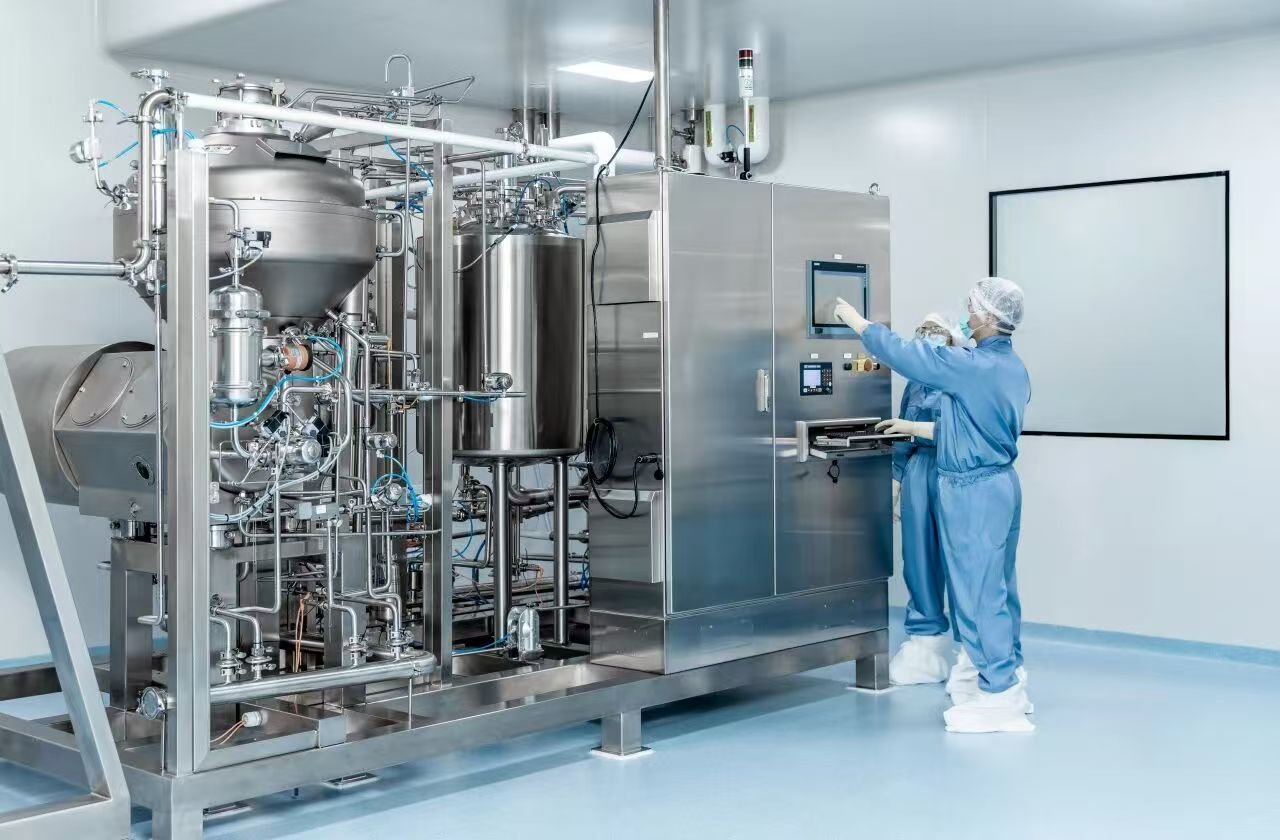
Our complete recombinant protein bioprocessing equipment design system consists of four interconnected workflow-centric modules covering full upstream-to-downstream production chains: expression & fermentation equipment design, buffer & medium preparation system design, downstream purification skid design, and sterile storage & transfer unit design. The expression module features low-shear bioreactors and fermenters with precisely optimized aeration, stirring and feeding strategies, adapting to both prokaryotic fermentation and eukaryotic cell culture to maximize protein expression titer and cell viability. The buffer preparation module includes customized multi-stage mixing tanks, automatic powder feeding systems and constant-temperature circulation units, ensuring consistent buffer pH, conductivity and purity for stable chromatographic performance. The purification skid module integrates tailor-sized chromatography frames, UF/DF ultrafiltration systems and virus filtration assemblies with customized flow paths to minimize protein loss and efficiently remove endotoxins and host impurities. The sterile storage module provides sealed, temperature-controlled sanitary vessels with full CIP/SIP coverage and closed sterile transfer interfaces to maintain protein stability before formulation.
4. Industrial Application & Full Lifecycle Engineering Support
This recombinant protein-focused equipment design is widely applied in greenfield protein manufacturing plant construction, brownfield production line upgrading, process optimization for existing protein platforms and new recombinant protein pipeline development projects. All modular designs retain excellent scalability, supporting seamless linear scale-up from lab-scale process screening to commercial mass production without major equipment structural modification or process rework. We provide full-lifecycle technical services including pre-sales process matching design customization, structural optimization consultation, factory FAT performance verification, on-site SAT commissioning, operational training and long-term technical iteration support. By embedding recombinant protein biochemical characteristics into every equipment detail, our design ensures stable protein activity, high purification recovery and consistent batch quality, helping biopharma clients accelerate process scale-up, reduce production costs and achieve rapid industrialization of recombinant protein therapeutics.