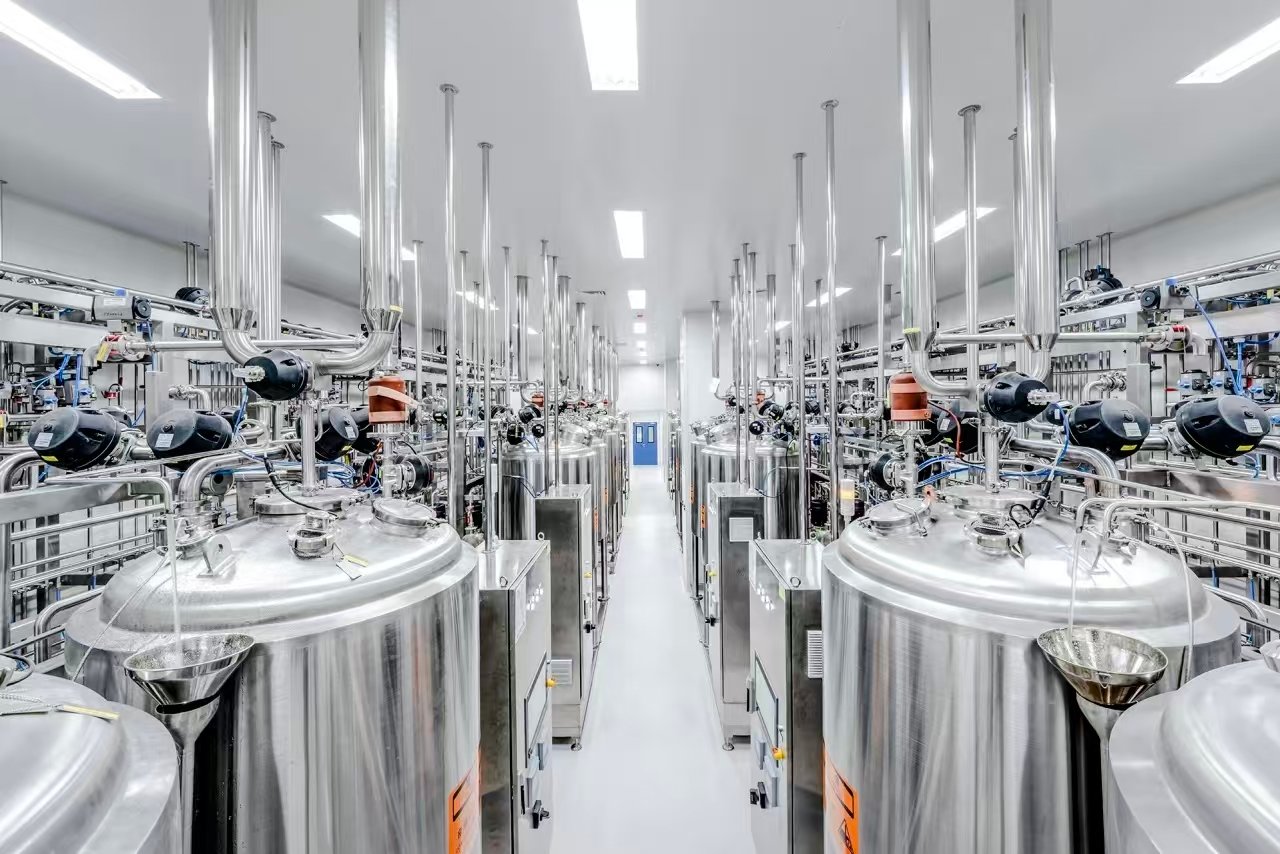
1. Product Positioning & Industry Overview
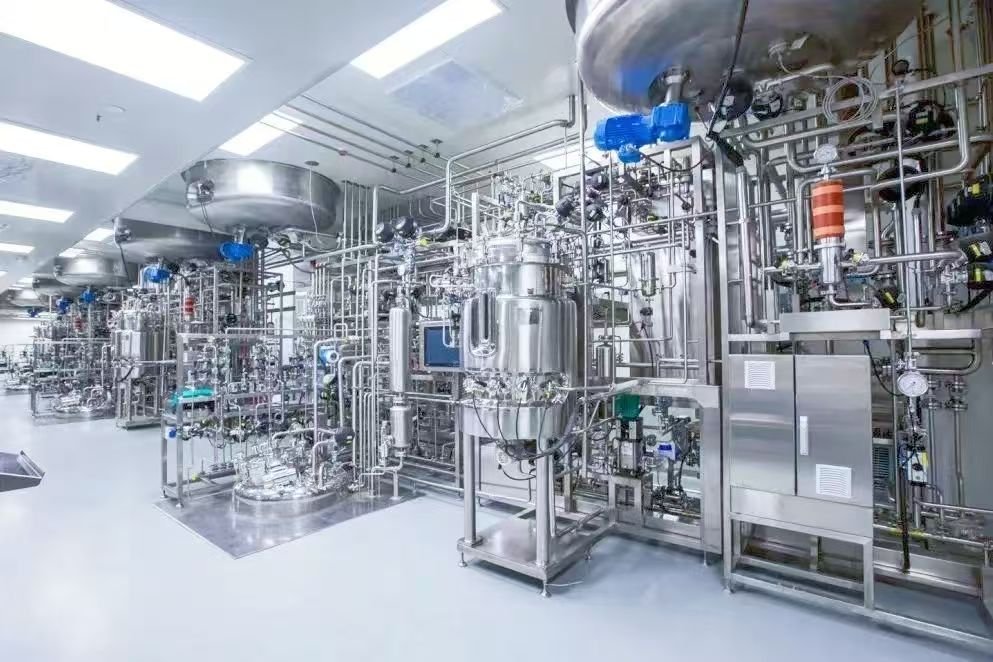
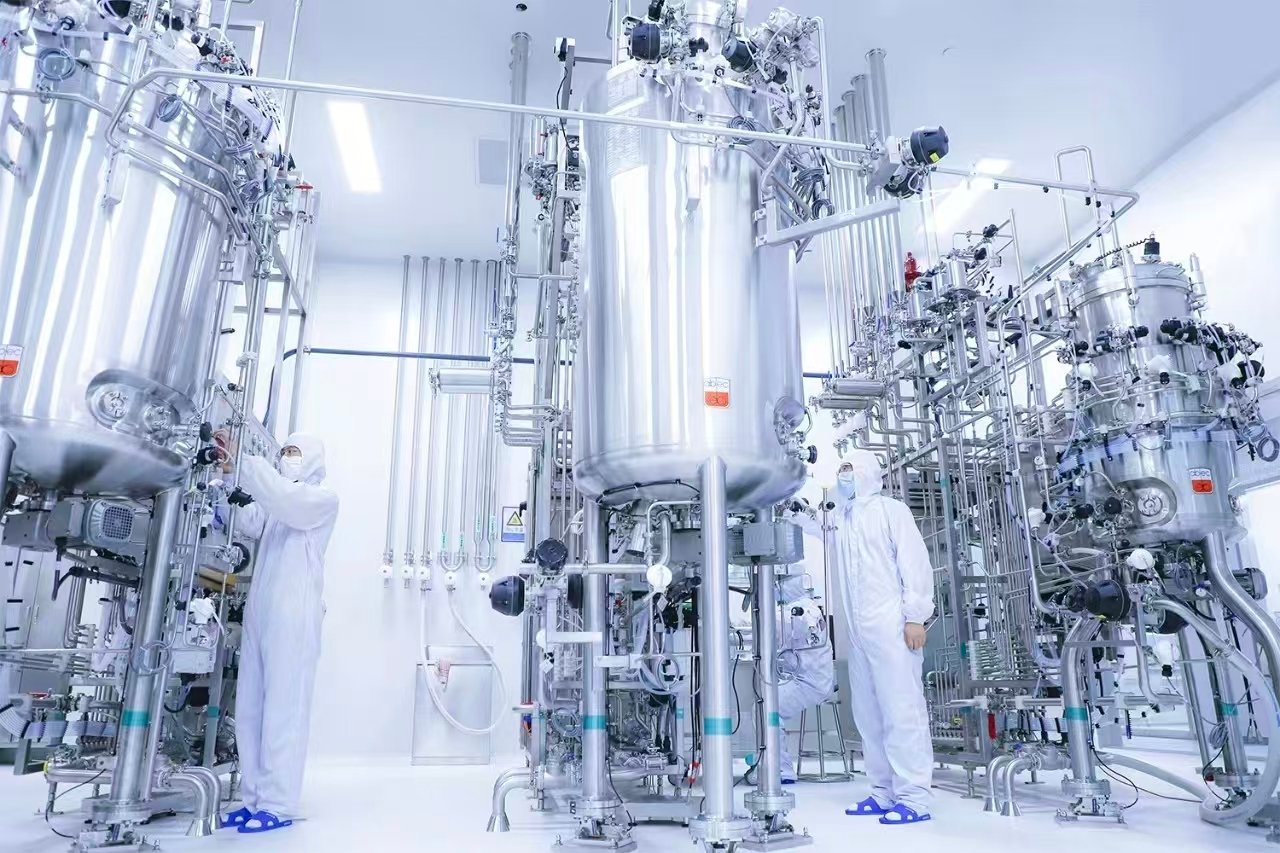
Engineered for large-scale standardized microbial biomanufacturing and high-activity industrial enzyme commercial industrialization, our Enzyme Preparation Fermentation and Downstream Purification Plant Design delivers full-process integrated engineering solutions for GMP-compliant commercial enzyme production facilities. Serving as the core systematic process architecture that governs strain metabolic stability, enzyme activity consistency, impurity exclusion and end-product purification qualification, our specialized turnkey plant design resolves inherent industry pain points including uncontrollable fermentation metabolism, low enzyme titer, inefficient downstream impurity removal, enzymatic activity attenuation during purification, and fragmented upstream-downstream process linkage. Customized for industrial enzyme preparations, food-grade enzymes, feed enzyme additives and bio-catalytic raw material manufacturing, our design framework strictly aligns with global industrial bioprocess specifications and biomanufacturing GMP protocols, covering full-lifecycle engineering implementation from upstream fermentation layout optimization and midstream crude separation configuration to downstream fine purification, concentration and finished-product stabilization processing.
2. Core Design & Technical Framework
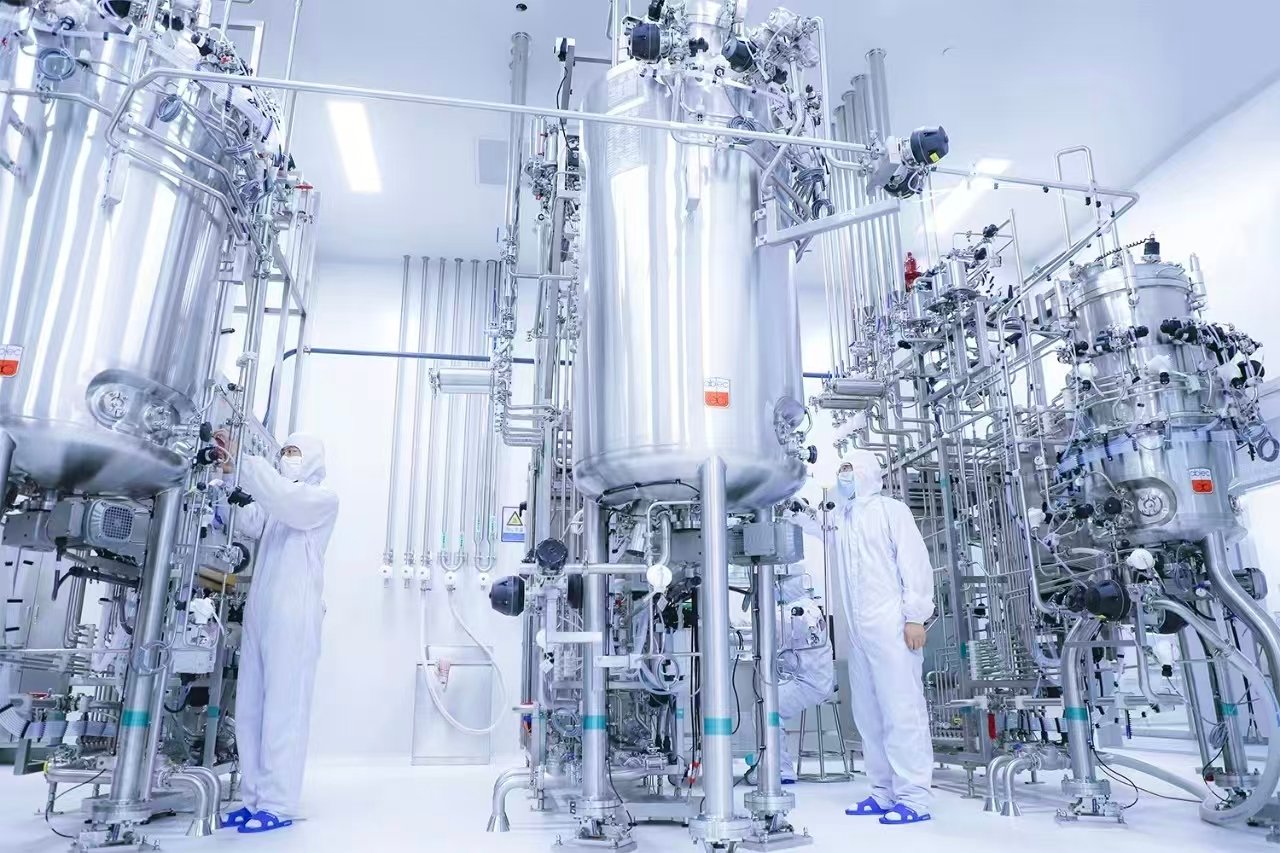
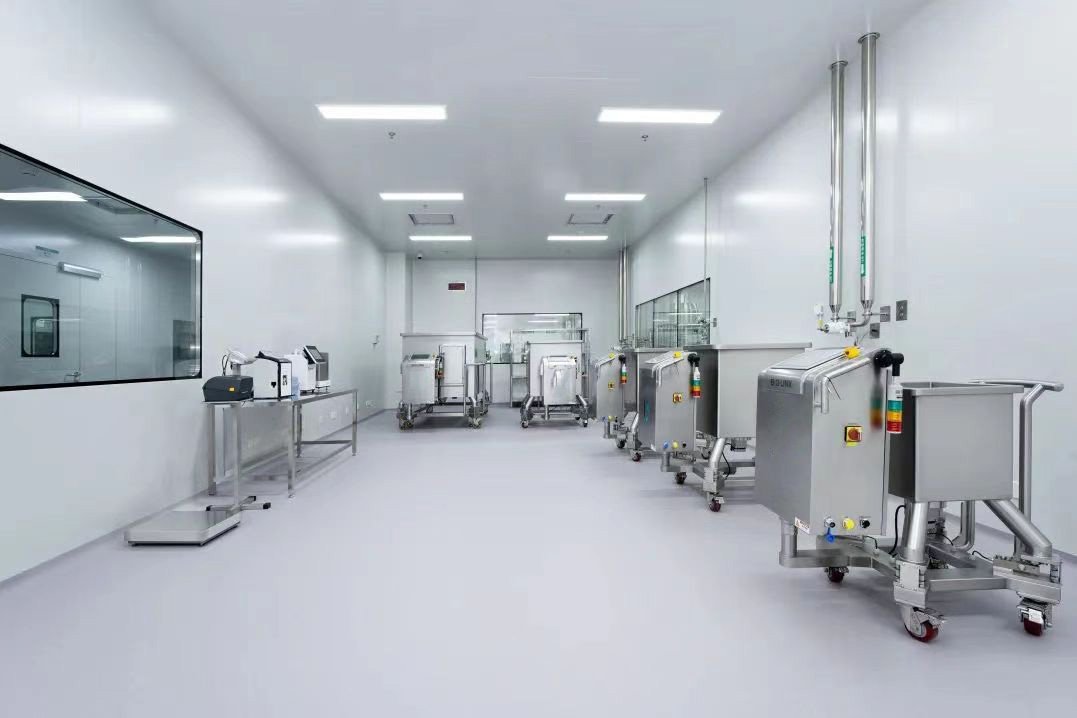
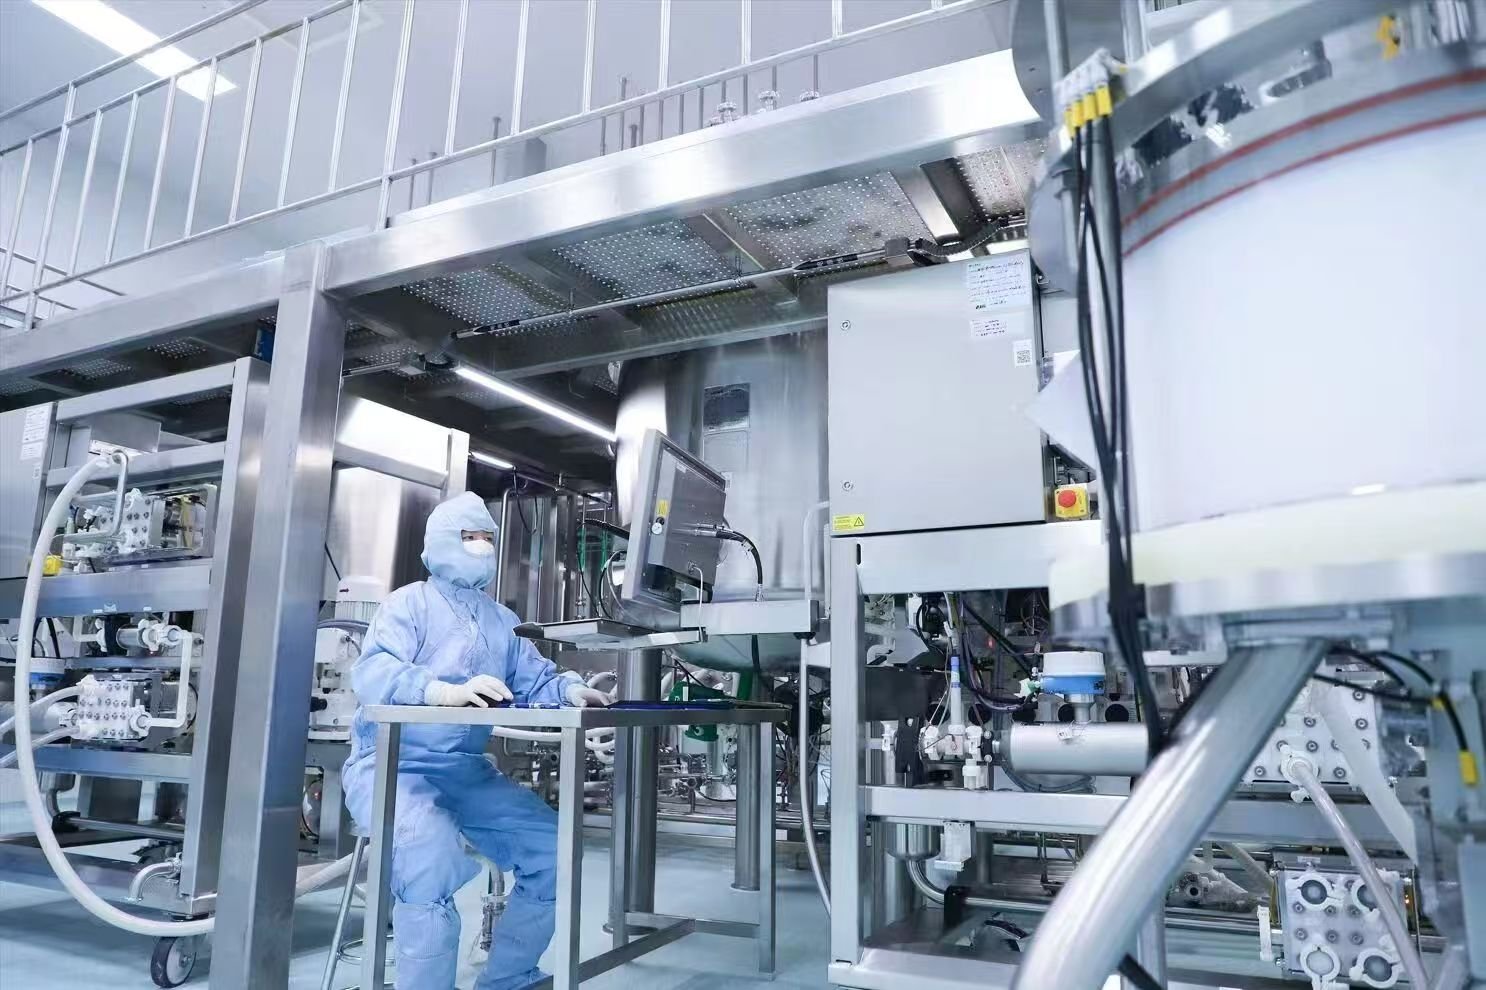
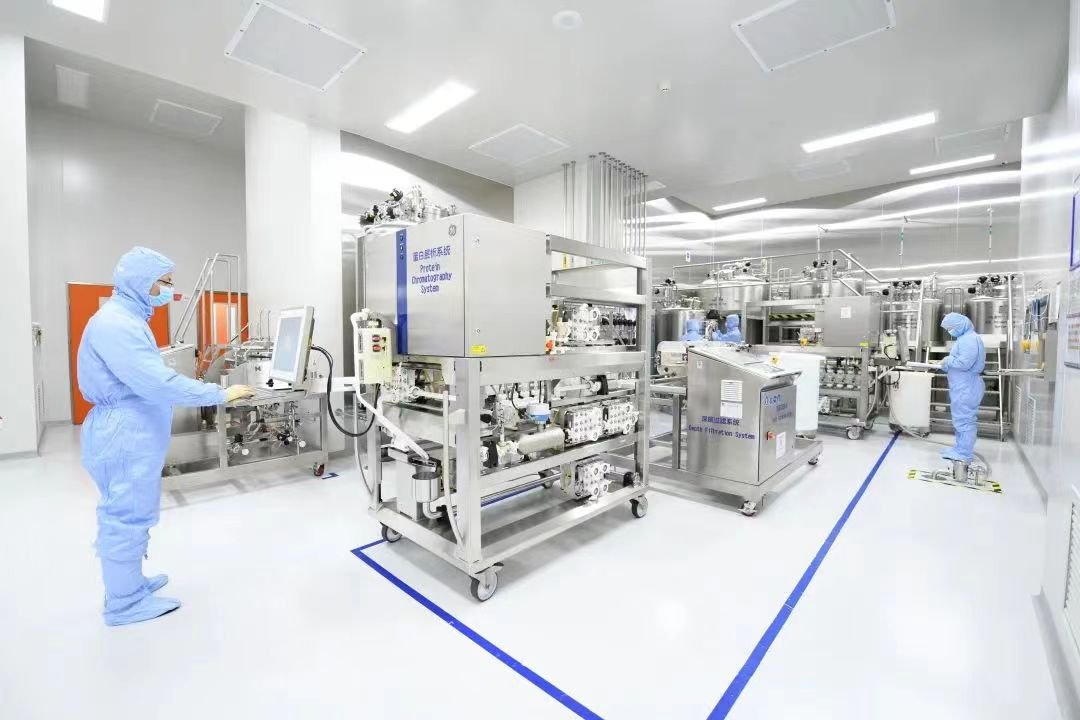
Adhering to stringent Quality by Design (QbD) paradigms and industrial microbial manufacturing benchmarks, our full-spectrum plant engineering integrates upstream seed strain activation, high-density aerobic submerged fermentation, intermediate solid-liquid separation, multi-stage chromatographic and membrane purification, enzymatic concentration and stable finished-product formulation workflows. We adopt scientific segmented process zoning and hierarchical sterile isolation mechanisms to fully segregate strain amplification, industrial fermentation, crude broth clarification, fine purification and enzyme preparation molding zones, comprehensively mitigating cross-contamination, heterologous microbial intrusion and enzymatic denaturation risks. The entire plant production system features a low-shear, temperature-controlled and enzyme-friendly operational logic, with customizable parameter calibration tailored for aerobic fermentation and bioactive substance purification. Supporting uninterrupted sterile material transfer, intelligent parameter dynamic iteration and modular capacity expansion, the system achieves seamless compatibility with automated CIP/SIP units, intelligent environmental monitoring platforms and closed-loop purification conveying systems, establishing a robust, traceable and fully standardized industrial enzyme manufacturing ecosystem.
3. Premium Performance & Technical Advantages
Distinct from conventional fragmented enzyme production plant layouts with disjointed process units, our integrated fermentation and downstream purification engineering solution delivers differentiated technical advantages in bioactivity retention rate, process continuity and batch-to-batch reproducibility. The optimized staged fed-batch fermentation strategy stabilizes microbial metabolic kinetics and maximizes unit volumetric enzyme yield, while graded downstream purification technology efficiently eliminates metabolic residues, heterologous proteins and particulate impurities without compromising target enzymatic activity. Customized temperature and pressure-controlled purification workflows minimize bioactive denaturation and structural attenuation, enabling superior enzyme activity retention and uniform end-product quality consistency. All process parameters, sanitary design criteria and operational SOPs fully comply with industrial GMP and food-grade biomanufacturing regulatory requirements, supporting full-chain data traceability and standardized quality governance. The highly automated integrated configuration minimizes manual intervention and operational deviations, significantly compresses production lead time, reduces long-term operational and consumable costs, and sustains stable enzymatic activity across commercial-scale batch production.
4. Application Value & Industrial Empowerment
Our full-process enzyme preparation plant engineering serves as the fundamental technical infrastructure for standardized, scalable and high-quality industrial enzyme biomanufacturing. Widely applicable in greenfield enzyme production plant construction, conventional microbial fermentation facility upgrading, industrial biocatalyst production line renovation and high-standard bio-manufacturing base deployment, our engineering solutions empower enterprises to build high-activity, low-impurity, risk-controlled and audit-ready enzyme preparation manufacturing systems. By optimizing full bioprocess workflow logic, realizing seamless synergy of upstream fermentation and downstream purification core units, and standardizing whole-process quality control and bioactivity stabilization mechanisms, we effectively eliminate production uncertainties and reduce product defect rates. This enables biomanufacturing enterprises to achieve stable capacity scaling, flexible enzyme product pipeline iteration and standardized industrial upgrading, solidifying differentiated core competitiveness in the highly competitive global industrial enzyme and bio-catalytic manufacturing market.