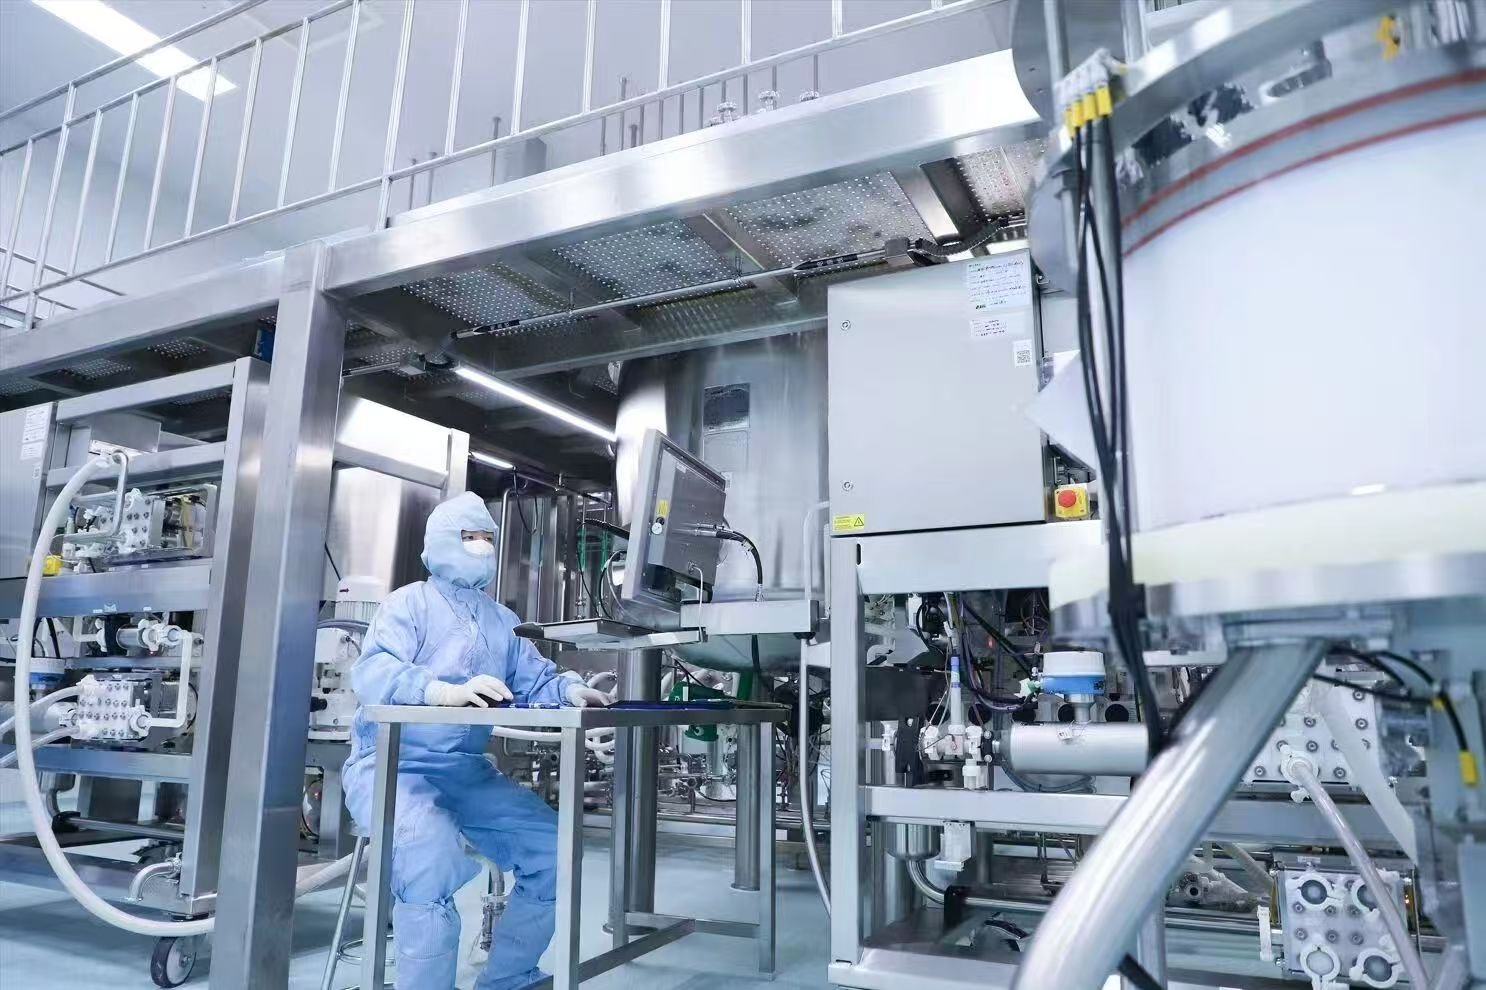
1. Product Overview & GMP Compliance Standards
Our large-scale bioprocessing equipment portfolio is a fully integrated, GMP-compliant manufacturing system specially engineered for commercial-scale monoclonal antibody production, covering the complete upstream and downstream workflow from seed cell amplification, high-density cell culture, crude harvesting, chromatographic purification to final formulation preparation. The entire equipment suite is designed and validated in strict accordance with FDA cGMP, EMA GMP and ICH Q8/Q9/Q10 quality guidelines, supporting stable, continuous and reproducible large-batch antibody biomanufacturing. Tailored to the high-standard quality requirements of antibody drugs, including low impurity residue, high product activity and strict batch consistency, the system effectively resolves common industrial bottlenecks such as limited production capacity, low expression titer, unstable purification yield and frequent process deviations, forming an audit-ready industrial manufacturing solution for antibody commercialization.
2. Core Technical Design & Industrial Advantages
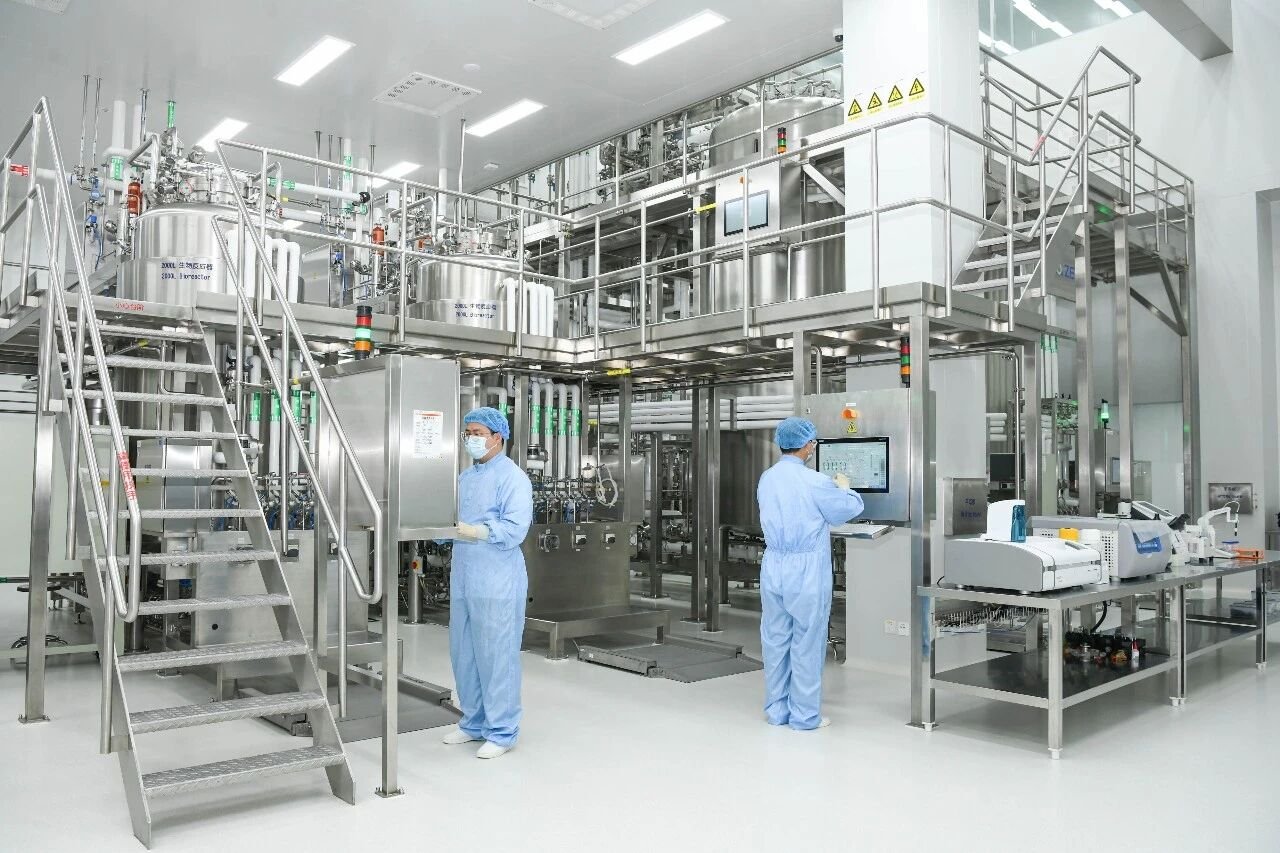
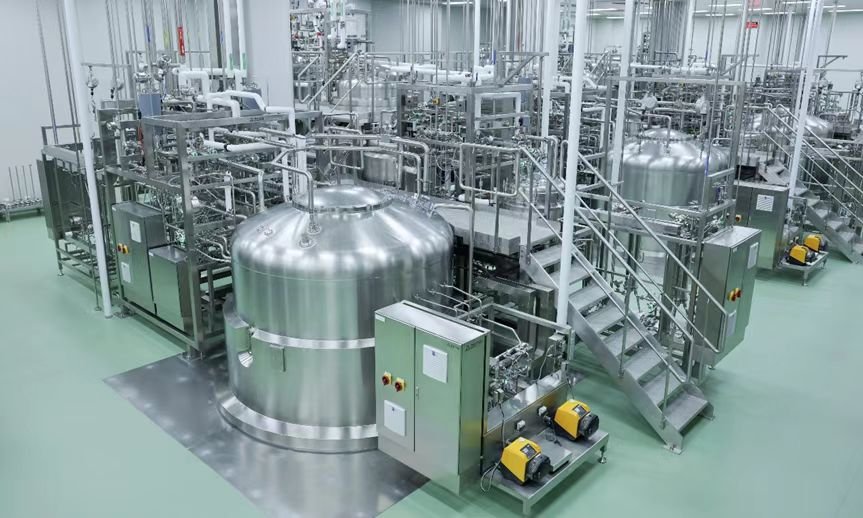
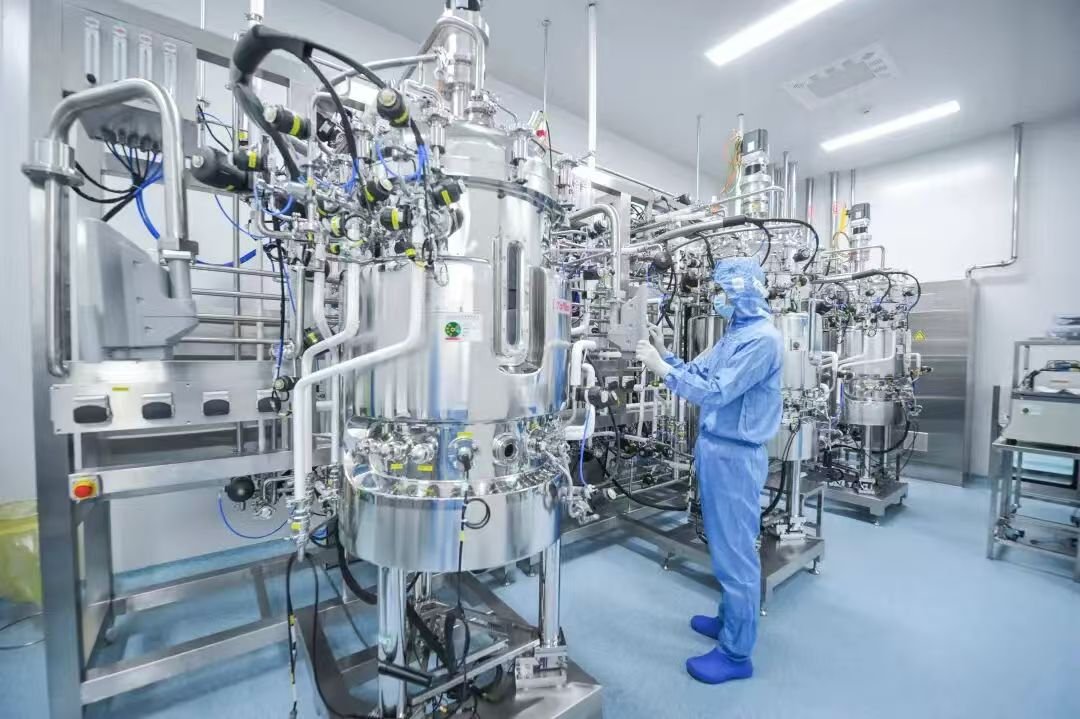
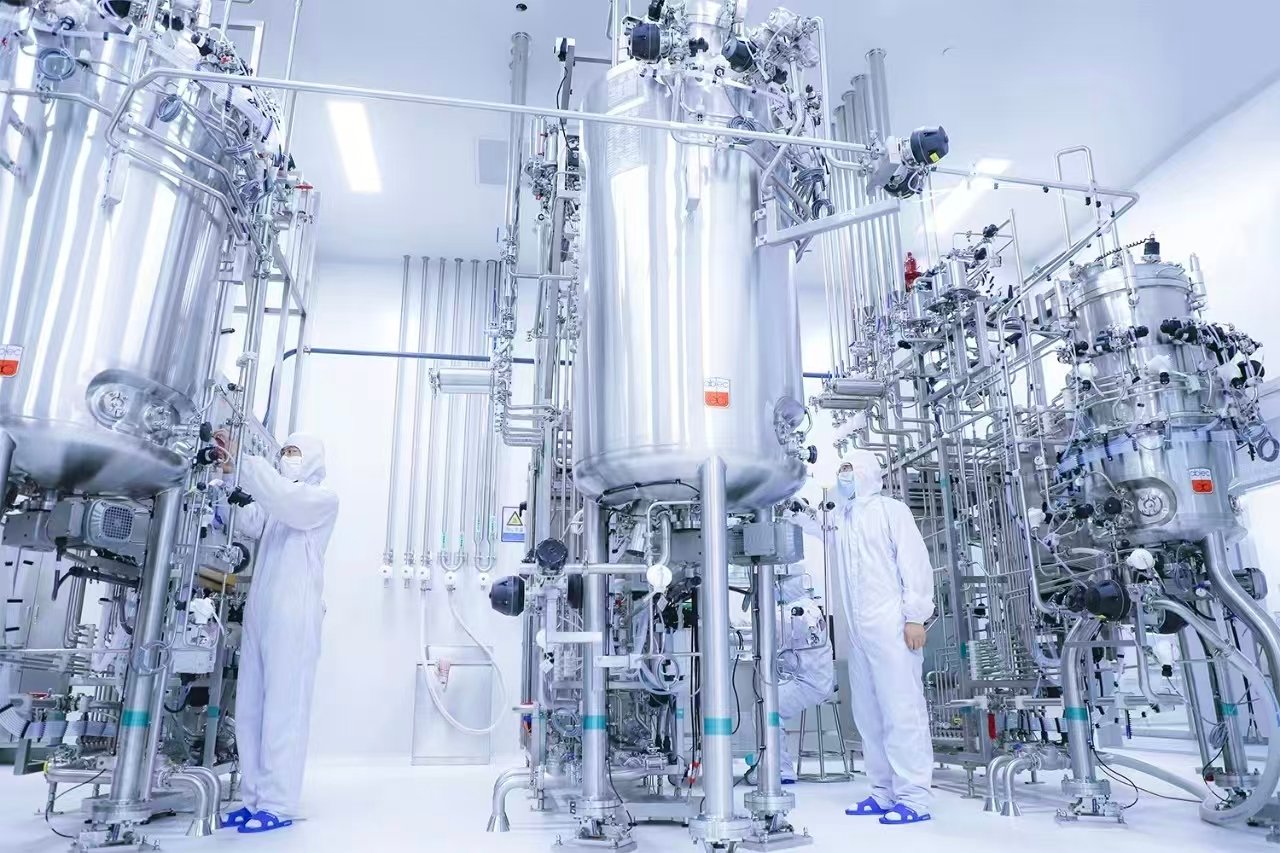
Adopting risk-based quality control and process-driven deterministic design philosophy, our large-scale antibody bioprocessing equipment focuses on stabilizing critical process parameters (CPPs) and sustaining consistent critical quality attributes (CQAs) throughout full production runs. The upstream core bioreactor system optimizes oxygen mass transfer, shear force control and nutrient feeding strategies to support high-density mammalian cell culture and high-level antibody expression, significantly improving unit production efficiency. The downstream integrated purification equipment adopts standardized chromatographic process logic, realizing efficient removal of host cell proteins, DNA residues, viruses and miscellaneous aggregates while maximizing target product recovery rate. All core units feature closed sterile operation structure, zero-dead-angle sanitary design and full-process automated parameter adjustment, minimizing manual intervention and human-induced contamination risks. Compared with conventional pilot-scale equipment, this industrial-grade portfolio delivers superior process robustness, scalability and batch-to-batch consistency for large-volume antibody manufacturing.
3. Full-system Functional Modules & Standard Configuration
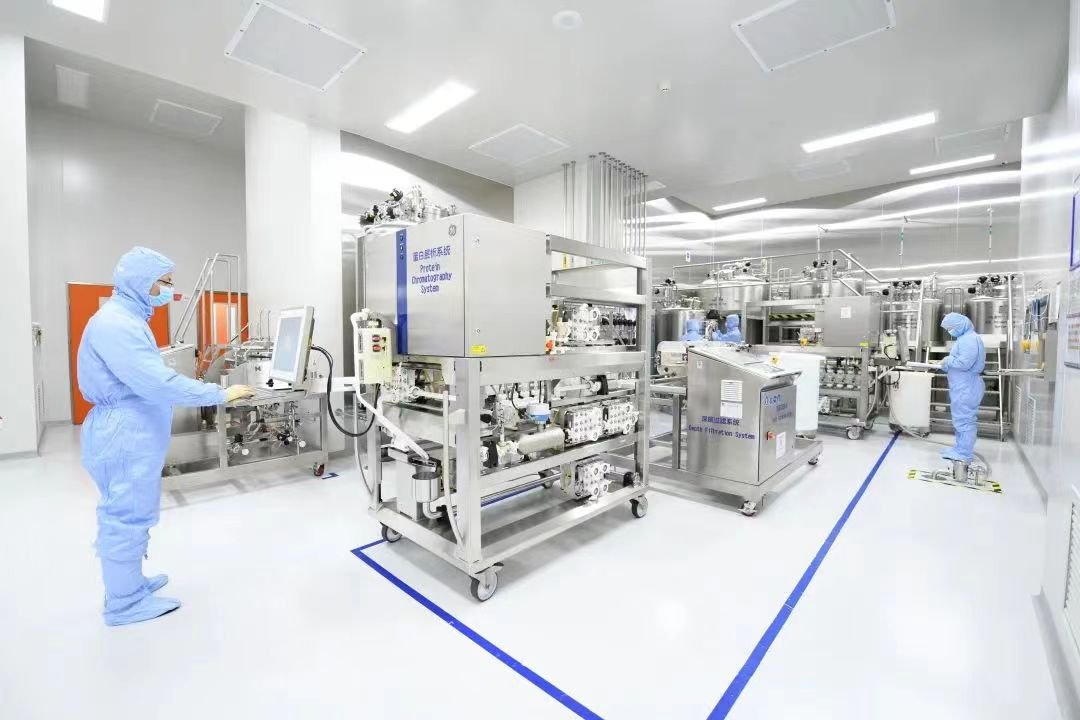
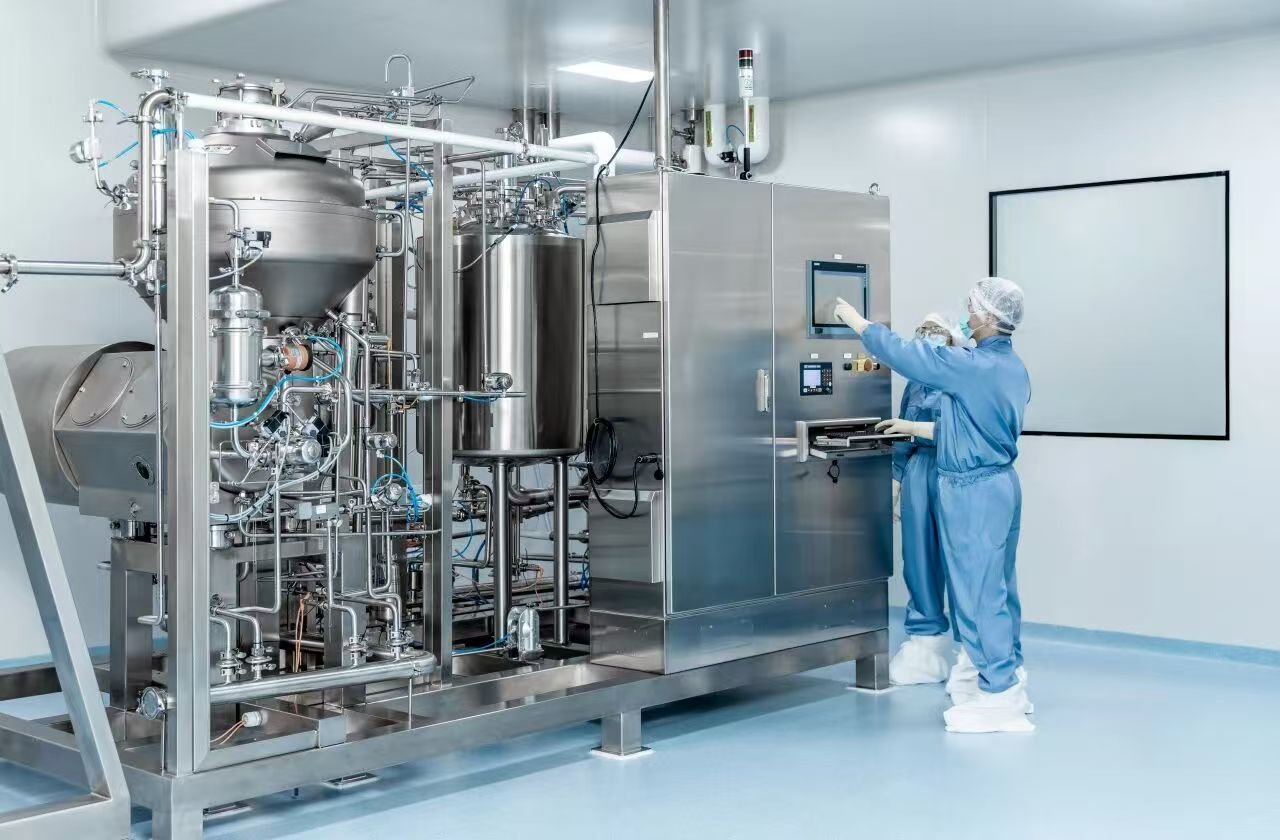
The complete large-scale antibody bioprocessing system consists of four core functional modules: upstream cell culture and fermentation unit, automated medium preparation and sterile transfer unit, downstream multi-stage purification unit, and auxiliary monitoring & utility support unit. The upstream module includes multi-stage seed bioreactors and large-scale production bioreactors, supporting linear scale-up from pilot scale to commercial manufacturing scale. The medium preparation and transfer module integrates automated batching, online parameter detection and closed aseptic delivery, providing stable and consistent culture conditions for cell growth. The downstream purification module covers protein A affinity chromatography, ion exchange polishing, ultrafiltration and diafiltration systems, achieving high-purity antibody refinement. All equipment is equipped with industrial PLC automatic control systems, supports one-key CIP and SIP sterilization, and realizes real-time data acquisition, recording and traceability, fully complying with industrial automated production and regulatory data integrity requirements.
4. Industrial Application & Full Lifecycle Service Support
This large-scale bioprocessing equipment portfolio is widely deployed in commercial monoclonal antibody manufacturing bases, large-scale biopharmaceutical production parks and antibody drug industrialization upgrading projects. It adapts to long-term continuous industrial production and multi-batch cyclic manufacturing scenarios, effectively expanding production capacity, reducing unit production costs and improving product qualification rates. With highly modular and scalable design, the equipment reserves sufficient expansion space for subsequent process optimization, titer improvement and production line capacity upgrade. We provide full lifecycle engineering services including process scheme customization, equipment integration debugging, GMP validation document compilation, personnel operation training and long-term after-sales technical support, helping biopharmaceutical enterprises rapidly realize stable commercial production of antibody drugs and enhance core market competitiveness in standardized global biomanufacturing.