





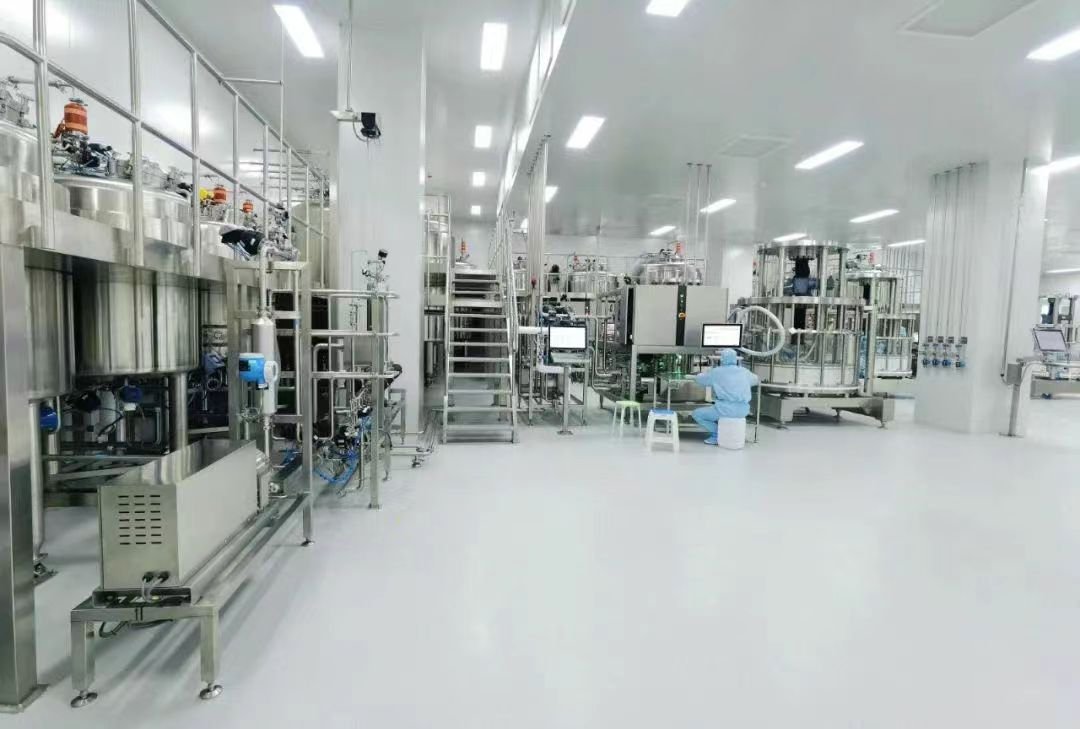
Blow-Fill-Seal (BFS) denotes an integrated manufacturing process encompassing blow molding, filling and sealing. BFS equipment is an automated system that thermoforms thermoplastic feedstock into containers, performs product filling and achieves hermetic sealing in a continuous operational sequence. As blow molding, filling and sealing are integrated and executed on a single machine, the technology is also referred to as the “three-in-one” process.
The core principle of BFS technology begins with polymer plasticization. Thermoplastic feedstock, generally in granular pellet form, is heated and melted into a flowable, malleable melt, then extruded under pressure into molds. The melt cools and solidifies to yield finished plastic components. For pharmaceutical BFS production, medical-grade polyolefin pellets complying with defined bioburden and endotoxin specifications are adopted. These non-cytotoxic feedstocks are compatible with BFS extrusion operations. Common materials include polypropylene (PP), high-density polyethylene (HDPE) and low-density polyethylene (LDPE. Pellets generally do not require pre-sterilization. Materials are conveyed via vacuum feeding into a screw extruder. Utilizing the thermal softening characteristics of thermoplastics: PP exhibits a melting point of 130–170°C, HDPE 130–140°C, and LDPE 110–130°C. Inside the extruder, pellets are processed at temperatures exceeding 170°C and pressures above 20 MPa. Subjected to high temperature, compression and shear forces, pellets are homogenized, compacted and melted. This plasticization stage simultaneously achieves thermal decontamination, generating sterile molten polymer. The melt exits through the extruder die head to form a continuous, hollow, thickness-controlled tubular parison. Sterile compressed gas is injected into the parison lumen to prevent inner surface collapse and adhesion. This tubular preform, known as the parison, serves as the precursor of the final molded container.
Conversion of the hot parison into finished containers is realised via blow molding and/or vacuum forming. After the hot parison enters the mold cavity, a custom-engineered mandrel (integrated filling nozzle assembly) delivers sterile compressed air to expand the parison; mold cavity vacuum may be applied to assist shaping. Combined internal pressurization and external vacuum stretch the parison to conform fully to the mold cavity geometry. BFS forming molds incorporate internal cooling channels circulating chilled water (8–16°C). Upon contact with cold mold surfaces, the expanded parison rapidly cools and solidifies into dimensionally consistent plastic containers with uniform wall thickness. Chilled water circulation stabilizes the forming process. Throughout container fabrication, the bottle neck and internal headspace are continuously protected by sterile gas under positive pressure, establishing a localized Grade A aseptic environment to facilitate filling. Upon completion of filling, mold closure induces thermal fusion to achieve hermetic sealing of the container neck.
Functioning as a compact, self-contained miniaturised production unit, BFS equipment executes and monitors all blow-fill-seal operations automatically with a small footprint. Compared with conventional glass container workflows, plastic pellet feedstock requires substantially reduced warehouse and staging capacity. Plastic containers deliver distinct advantages including light weight, shatter resistance and ease of administration. From the perspective of overall production economics and product quality assurance, BFS aseptic filling presents unique strengths relative to traditional aseptic filling lines. BFS technology is widely deployed for ophthalmic preparations, respiratory care products and selected injectable formulations. Nevertheless, multiple technical risks require targeted mitigation during BFS implementation.
Process Selection for Aseptic Manufacture of Sterile Products
It is universally acknowledged that sterile pharmaceutical manufacturing must minimise contamination risks originating from microorganisms, particulate matter and endotoxins. Contamination control constitutes a persistent priority and technical challenge throughout aseptic production. Two primary manufacturing routes are available for sterile medicinal products: terminally sterilized products, and aseptically processed products where partial or all unit operations adopt aseptic workflows. A sterile product is defined as a preparation free from viable microorganisms; however, absolute sterility cannot be guaranteed or verified via testing for any production batch. The sterility status of a batch is described probabilistically by the Probability of a Nonsterile Unit (PNSU) or Sterility Assurance Level (SAL). Products manufactured via terminal sterilization must achieve a PNSU not exceeding 10⁻⁶. For non-terminally sterilized products manufactured via aseptic processing, media fill simulation is mandatory. If one contaminated unit is detected when more than 10,000 units are filled, a formal investigation shall be initiated; identification of two contaminated units mandates investigation followed by re-qualification.
Terminal sterilization delivers superior sterility assurance. Where active pharmaceutical ingredients remain thermally stable under humid heat conditions, terminal moist heat sterilization shall be prioritised. Maintaining products at 121°C for 15–30 minutes readily achieves a PNSU below 10⁻⁶. Aseptic processing is only selected for heat-labile formulations or products incompatible with terminal sterilization. Under such circumstances, BFS represents one of the optimal technical solutions.
BFS Equipment Selection
BFS systems are categorised into shuttle-type (open parison) and rotary-type (closed parison) configurations based on whether the parison is exposed to ambient air. Conventional shuttle-type systems adopt a dedicated mandrel for blowing and filling without integration with the extruder head. The forming mold shuttles reciprocally between the extrusion station and mandrel station. Following extrusion, the mold closes to seal the parison bottom, and a hot cutting blade severs the parison top, generating an open preform exposed to surrounding air. The open parison is then transferred to the mandrel, which descends into the parison to perform blow/vacuum forming and filling. The mandrel retracts before thermal sealing of the container neck.
A prominent limitation of shuttle-type BFS is temporary open exposure of the parison. Cutting operations and mold transfer generate particulate debris. Vacuum forming may induce inward air ingestion as the internal container volume expands. To maintain aseptic integrity, the exposed zone must be protected by a Grade A air shower enclosure with rigorously controlled airflow patterns. The parison interior is maintained under positive pressure to displace ambient air and prevent ingress of particulates and microorganisms. Shuttle-type systems can be configured as a “one extruder, two mandrels” layout to boost throughput, matching slower forming and sealing rates with faster extrusion output.
The optimised rotary-type BFS, also termed closed parison equipment, integrates the filling nozzle and air supply channels concentrically within the combined extrusion mandrel assembly: the outer annulus serves as the melt flow channel, the middle channel delivers blowing gas, and the innermost lumen accommodates the filling needle. After parison formation, cutting is unnecessary; blowing and filling operations proceed entirely within the intact parison. All operations including forming, filling and sealing are completed within a continuously enclosed aseptic volume. The sealing cycle achieves dual functionality: the lower fused section forms the sealed top of the filled container, while the upper fused section acts as the bottom seal of the subsequent parison. Rotary BFS establishes a fully enclosed Grade A microenvironment and eliminates the requirement for the Grade A air shower system mandatory for shuttle-type units. During routine production, the blowing and filling assembly remains enclosed within the parison, ensuring the internal microenvironment of preforms and finished containers stays continuously sterile. The aseptic environment surrounding the filling mandrel is equivalent to the internal headspace of hermetically sealed finished products.
Cleanroom Classification for Filling Suites
Owing to high system integration, compact continuous workflows and seamless operational sequence, BFS equipment minimises open exposure area and duration within the critical Grade A zone, approaching near-zero open exposure. Accordingly, the background cleanroom classification for filling suites producing non-terminally sterilized products does not mandate Grade B; Grade C is acceptable without compromising sterility assurance.
Regulatory specifications stipulate: BFS equipment for non-terminally sterilized products shall be fitted with integral Grade A air shower systems. Personnel shall adopt gowning appropriate for Grade A/B classified areas, and equipment shall be installed within at least a Grade C cleanroom. Static airborne particulate and microbial levels shall comply with defined specifications; microbial limits shall be sustained under dynamic operating conditions. Supported by Clean-in-Place (CIP) and Steam-in-Place (SIP) capabilities, BFS significantly reduces contamination risks for non-terminally sterilized sterile products.
Featuring high-level automation with continuous real-time monitoring of temperature, pressure, line speed, differential pressure, airborne particles, viable bioburden and airflow velocity, a typical BFS filling suite only requires one to two operators. Minimal inherent and corrective interventions are required within the Grade A zone, and operator activities within classified areas are limited. Given that human operators constitute the dominant contamination source, BFS minimises reliance on manual intervention through automation and system integration, substantially elevating sterility assurance performance compared with traditional aseptic filling lines.
BFS technology can also be deployed for terminally sterilized products. Thanks to minimal open exposure area and duration, inherent contamination risk remains low. Regulatory requirements are accordingly relaxed: BFS equipment for terminally sterilized products shall be installed within at least a Grade D cleanroom.
Selection of Plastic Pellet Materials
Regulatory guidelines prioritise terminal sterilization for sterile pharmaceuticals where technically feasible. If formulations tolerate thermal stress, packaging materials capable of withstanding 121°C moist heat sterilization shall be selected. Based on melting point characteristics, PP and HDPE are suitable for terminal sterilization, whereas LDPE is generally not recommended. For heat-sensitive formulations incompatible with terminal sterilization, non-terminal aseptic processing is adopted, and LDPE becomes a viable candidate material. LDPE delivers favourable moldability and produces flexible containers suitable for squeezing and easy opening.
As molded plastic containers function as primary packaging with direct contact with pharmaceutical products, material selection must evaluate safety and extractables-leachables compatibility. The polymer must not release foreign substances, adsorb active pharmaceutical ingredients, or trigger chemical interactions that undermine formulation stability. Transparent grades are generally preferred to facilitate visual inspection of product appearance, visible particles and subvisible particulates. Opaque or semi-transparent grades may be specified for light-sensitive formulations. For manually squeezable presentations such as eye drops, adequate container flexibility and optimised opening force are required. For connected unit-dose containers, controlled separation force between individual units shall be validated.
Compared with glass, plastic exhibits inferior gas barrier performance and variable permeability. A general inverse correlation exists between moldability and barrier properties: PP delivers superior barrier performance over HDPE, which outperforms LDPE. Even low-level permeability may compromise product stability, especially for oxidation-sensitive formulations requiring inert gas blanketing. Additional barrier layers such as aluminium foil overwrap can be applied to approximate the barrier performance of glass containers.
For ophthalmic and respiratory formulations, squeeze flexibility is prioritised, rendering LDPE the dominant material. HDPE is commonly adopted for storage containers. PP is specified where enhanced chemical resistance, improved barrier performance or higher thermal stability is required. Environmental factors including recyclability and degradability should also be evaluated during pellet feedstock selection.
Supplementary Design Considerations
In-line melt forming leaves residual heat on freshly molded container walls despite rapid mold cooling. Thermal sealing further elevates liquid temperature inside filled containers. For rotary-type BFS, the filling nozzle is integrated with the hot extruder mandrel. Cooling jackets must be implemented on the mandrel assembly to mitigate heat transfer to liquid formulations. Through equipment design optimisation, enhanced mold cooling and process parameter tuning, local temperature rise of liquid product is generally controlled within 5–10°C above ambient filling suite temperature, with rapid temperature recovery within minutes. This transient temperature excursion poses minimal risk of thermal degradation to heat-sensitive products.
BFS equipment supports flexible installation layouts. Units can be fully housed within classified areas to facilitate observation; alternatively, wall-through installation enables segregation of clean-side and unclean-side zones to reduce classified area footprint and simplify maintenance. During cleanroom layout design, all non-critical operations shall be relocated outside classified areas wherever practicable. Trimming, printing, embossing and leak testing are preferably executed outside filling suites to minimise contamination sources. If trimming generates plastic waste within classified areas, dedicated waste transfer routes must be incorporated to rapidly remove debris.
BFS systems incorporate multiple 0.22 μm sterile filters for compressed air utilised in parison support, blow molding and Grade A air shower supply. Additional sterile filters are deployed for liquid formulation filtration. Filter integrity testing constitutes a mandatory control measure.
Where secondary components (e.g., caps) are assembled post-forming, components must undergo appropriate decontamination. For aseptic processes, assembly shall occur under Grade A conditions using pre-sterilised components. For terminally sterilized products, sterilization validation must confirm all critical contact surfaces between components and containers are effectively penetrated by sterilant, including challenging-to-reach zones. Validated test methods shall be established to verify reliable sealing between components and molded containers.
For formulations incompatible with sterile filtration or terminal sterilization (e.g., suspensions, high-viscosity solutions), alternative validated aseptic control strategies such as sterile compounding or pre-filling thermal decontamination shall be implemented.
Equipment qualification must address product quality assurance and contamination risk control, including thermal protection for heat-sensitive biomolecules (proteins, vaccines, biopolymers), airflow pattern design to prevent particulate ingress, environmental monitoring systems, and bioburden control for incoming polymer pellets. Key risk points include particulate generation during parison cutting and forming, contamination of critical filling headspace, and incomplete thermal sealing. Hydraulic and cooling circuits positioned adjacent to critical aseptic zones require robust safeguards to prevent fluid leakage and condensation, which represent major contamination hazards. All critical parameters governing seal integrity shall be identified, monitored and controlled, and 100% in-line leak testing using validated methodologies shall be implemented for thermally sealed BFS containers.
Illustrative Layout Example
The BFS workshop adopts a classic annular peripheral corridor as a Controlled Non-Classified (CNC) zone, facilitating personnel flow, material movement and emergency evacuation while achieving effective production observation with minimal operational disruption. The filling suite housing BFS equipment follows a Grade C background plus local Grade A configuration: the filling room is classified Grade C, and the critical aseptic exposure zone of each BFS unit is protected by integral Grade A laminar air showers.
The illustrative layout accommodates two BFS production lines. The first unit is fully installed within the classified area, enabling complete visual observation and simplified installation at the cost of an enlarged cleanroom footprint. The second unit adopts wall-through clean/unclean segregation: all operations involving exposed product (extrusion, forming, filling and sealing) reside inside the classified suite, while mechanical assemblies without product exposure are separated into an adjacent non-classified mechanical service room. A dedicated material transfer corridor serves the filling suite, with phased transfer operations executed via pass-through chambers. Ancillary classified spaces include a cleaning storage room and tool storage room.
The plastic pellet storage room adopts a Grade D background plus local Grade A design. The room maintains static Grade D classification with HEPA supply air, wall-mounted louver exhaust without air recirculation, and approximately 15 air changes per hour. Two stainless steel silos are positioned adjacent to the filling suite, serving the two BFS lines respectively. Sanitary vacuum conveying pipes transfer pellets from silos to each extruder. LDPE feedstock is selected for flexible single-dose plastic ampoules containing sterile liquid formulations.
To protect pellets from particulate, microbial and endotoxin contamination, each silo is covered by an FFU laminar flow hood providing positive pressure, forming a non-sterile glove box environment meeting static Grade A requirements for pellet exposure zones. Automated inclined conveyors reduce manual handling workload: externally disinfected pellet bags are transported upward to the Grade A enclosure. Operators access the enclosure via glove ports, cut open bags with sanitary blades, and allow pellets to gravity-feed into silos. Empty bags are immediately collected inside dedicated waste bins within the enclosure.
Liquid formulation preparation is split into two zones: Grade C compounding and Grade B+A compounding. This layout suits non-terminally sterilized formulations that cannot undergo sterile filtration (e.g., certain respiratory suspensions and high-viscosity liquids). Aseptic compounding for these products is complex and time-consuming. Given potential long-duration filling campaigns (12–24 hours), aseptic holding tanks are installed adjacent to the filling suite to store sterile bulk liquid, avoiding elevated bioburden risks arising from prolonged storage of non-sterile feedstock.
Material transfer between Grade C and Grade B compounding zones includes sealed process pipelines, double-door pulsating vacuum autoclaves, VHP sterilizers and air shower pass-through chambers. Moist heat sterilization is preferred for items transferred from Grade C to Grade B; VHP sterilization is deployed for heat-sensitive equipment. Air shower pass-through chambers are used for outgoing materials.
For personnel gowning design: operators for non-terminally sterilized BFS filling suites comply with Grade A/B gowning protocols. Separate exit gowning zones are assigned to filling operators and Grade B compounding operators. A shared sterile gowning room is provided for both workstreams, with laundry and garment storage positioned in proximity. This compact layout satisfies regulatory compliance, optimises space utilisation and minimises classified gowning area.
Conclusion
BFS technology emerged in the 1960s and has undergone continuous iterative optimisation. Its incorporation within GMP regulatory frameworks demonstrates that GMP constitutes a progressive scientific framework rather than rigid dogma. Conversely, tightening regulatory standards have driven sustained technical improvements to BFS equipment. Rotary-type BFS in particular minimises contamination risks from microorganisms, endotoxins and particulates. High-level system integration drastically reduces open exposure area, exposure duration and exposure frequency. Continuous automated monitoring of critical process and environmental parameters delivers a step-change advancement in aseptic manufacturing capability. It ranks among the most robust aseptic filling technologies for liquid formulations, offering an alternative to conventional Grade B+A and isolator-based workflows.
Previously, heat-labile sterile formulations unsuitable for terminal sterilization predominantly relied on lyophilisation lines equipped with vial washing, depyrogenation, filling and crimping stations. The maturation of BFS expands formulation development options and may become the mainstream solution for applicable product categories. Single-dose disposable plastic packaging delivers lightweight, convenient administration without preservatives. Thermal degradation risks associated with terminal sterilization are eliminated, safeguarding product safety and efficacy. Accordingly, BFS enjoys broad application prospects across pharmaceuticals, cosmetics and health food sectors.
